

132
4 Simulation of Transient Keyhole and Weld Pool
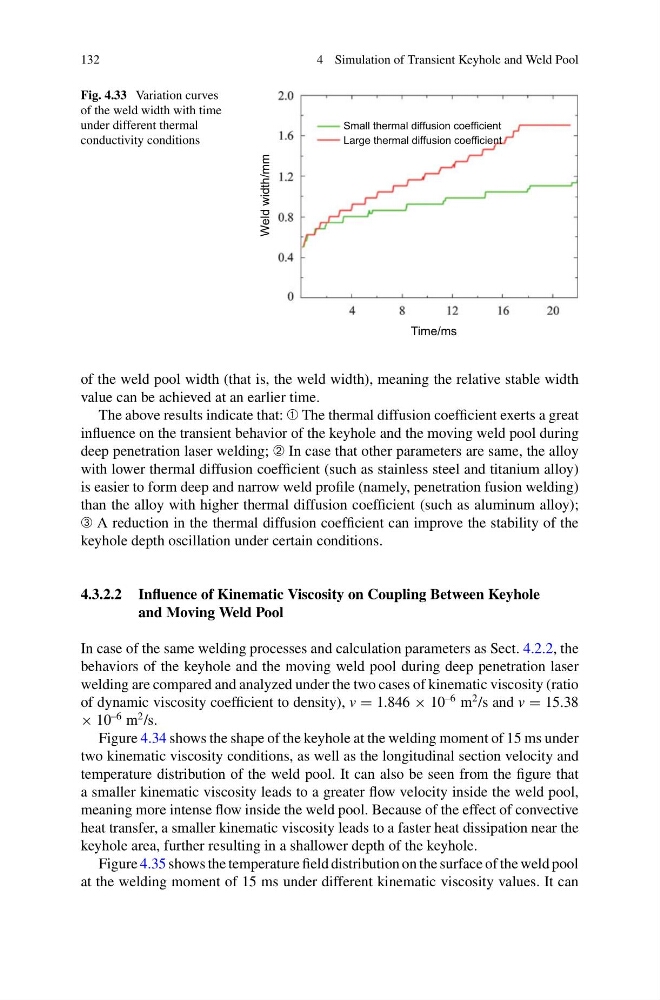
Fig. 4.33 Variation curves
of the weld width with time
under different thermal
conductivity conditions
Time/ms
Weld width/mm
Small thermal diffusion coefficient
Large thermal diffusion coefficient
of the weld pool width (that is, the weld width), meaning the relative stable width
value can be achieved at an earlier time.
The above results indicate that: ➀ The thermal diffusion coefficient exerts a great
influence on the transient behavior of the keyhole and the moving weld pool during
deep penetration laser welding; ➁ In case that other parameters are same, the alloy
with lower thermal diffusion coefficient (such as stainless steel and titanium alloy)
is easier to form deep and narrow weld profile (namely, penetration fusion welding)
than the alloy with higher thermal diffusion coefficient (such as aluminum alloy);
➂ A reduction in the thermal diffusion coefficient can improve the stability of the
keyhole depth oscillation under certain conditions.
4.3.2.2 Influence of Kinematic Viscosity on Coupling Between Keyhole
and Moving Weld Pool
In case of the same welding processes and calculation parameters as Sect. 4.2.2, the
behaviors of the keyhole and the moving weld pool during deep penetration laser
welding are compared and analyzed under the two cases of kinematic viscosity (ratio
of dynamic viscosity coefficient to density), v = 1.846 × 10
–6 m
2 /s and v = 15.38
× 10
–6 m
2 /s.
Figure 4.34 shows the shape of the keyhole at the welding moment of 15 ms under
two kinematic viscosity conditions, as well as the longitudinal section velocity and
temperature distribution of the weld pool. It can also be seen from the figure that
a smaller kinematic viscosity leads to a greater flow velocity inside the weld pool,
meaning more intense flow inside the weld pool. Because of the effect of convective
heat transfer, a smaller kinematic viscosity leads to a faster heat dissipation near the
keyhole area, further resulting in a shallower depth of the keyhole.
Figure 4.35 shows the temperature field distribution on the surface of the weld pool
at the welding moment of 15 ms under different kinematic viscosity values. It can