

424
12 Integration and Assembly Technology of Lunar Lander
Fig. 12.10 Photograph
taken by descent camera
during landing
Digital sampling
Shaped
multilayer design
and modification
Shaped multi-layer
Manufacture
Shaped
multilayer
review
Multi-layer
installation
Solder
connection
Wire
connection
Acquire Pro/E
model
Pro/E model
modification
Generate
stl file
Model surface
unfolded
Modify
unfolded
drawing
Multi-level
review
Installation
Stainless
steel high
temperature
protection
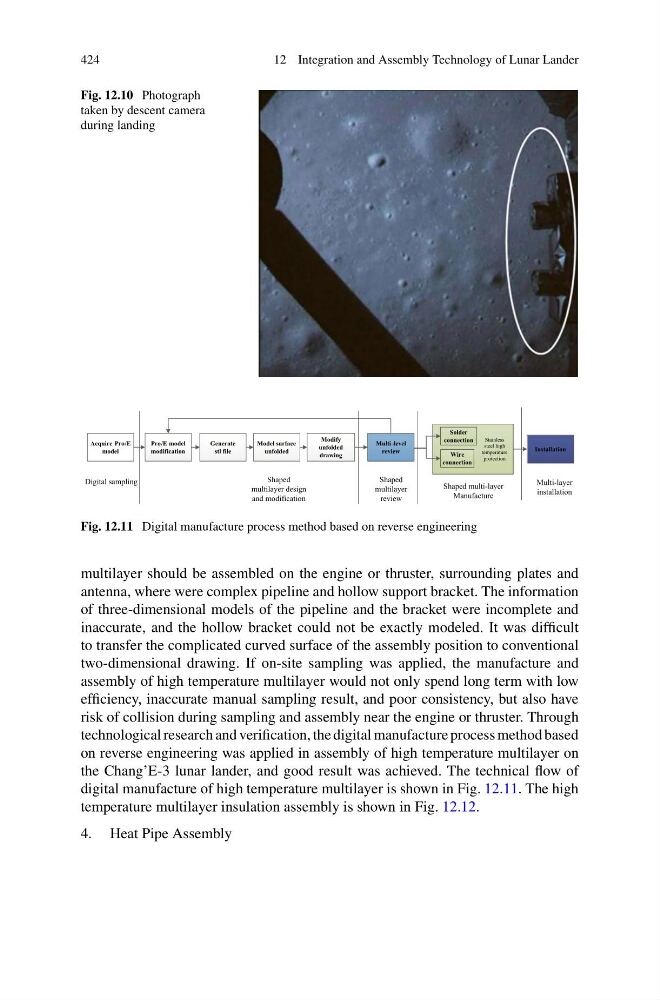
Fig. 12.11 Digital manufacture process method based on reverse engineering
multilayer should be assembled on the engine or thruster, surrounding plates and
antenna, where were complex pipeline and hollow support bracket. The information
of three-dimensional models of the pipeline and the bracket were incomplete and
inaccurate, and the hollow bracket could not be exactly modeled. It was difficult
to transfer the complicated curved surface of the assembly position to conventional
two-dimensional drawing. If on-site sampling was applied, the manufacture and
assembly of high temperature multilayer would not only spend long term with low
efficiency, inaccurate manual sampling result, and poor consistency, but also have
risk of collision during sampling and assembly near the engine or thruster. Through
technological research and verification, the digital manufacture process method based
on reverse engineering was applied in assembly of high temperature multilayer on
the Chang’E-3 lunar lander, and good result was achieved. The technical flow of
digital manufacture of high temperature multilayer is shown in Fig. 12.11. The high
temperature multilayer insulation assembly is shown in Fig. 12.12.
4. Heat Pipe Assembly