

554
The Chemistry and Technology of Petroleum
separation of wax as a liquid that is extracted at temperatures above the melting point of the wax
through preferential selectivity of the solvent. However, the former mechanism is the usual basis for
commercial dewaxing processes.
In the 1930s, two types of stocks, naphthenic and paraffinic, were used to make motor oils. Both
types were solvent extracted to improve their quality, but in the high-temperature conditions encountered in service, the naphthenic type could not stand up as well as the paraffinic type. Nevertheless,
the naphthenic type was the preferred oil, particularly in cold weather, because of its fluidity at
low temperatures. Previous to 1938, the highest quality lubricating oils were of the naphthenic type
and were phenol treated to pour points of −40°C to −7°C (−40°F to 20°F), depending on the viscosity of the oil. Paraffinic oils were also available and could be phenol treated to high-quality oil, but
their wax content was so high that the oils were solid at room temperature.
The lowest viscosity paraffinic oils were dewaxed by the cold press method to produce oils with a
pour point of 2°C (35°F). The light paraffin distillate oils contained a paraffin wax that crystallized
into large crystals when chilled and could thus readily be separated from the oil by the cold press
filtration method. The more viscous paraffinic oils (intermediate and heavy paraffin distillates)
contained amorphous or microcrystalline waxes, which formed small crystals that plugged the filter
cloths in the cold press and prevented filtration. Because the wax could not be removed from intermediate and heavy paraffin distillates, the high-quality, high-viscosity lubricating oils in them could
not be used except as cracking stock.
Methods were, therefore, developed to dewax these high-viscosity paraffinic oils. The methods
were essentially alike in that the waxy oil was dissolved in a solvent that would keep the oil in
solution; the wax separated as crystals when the temperature was lowered. The processes differed
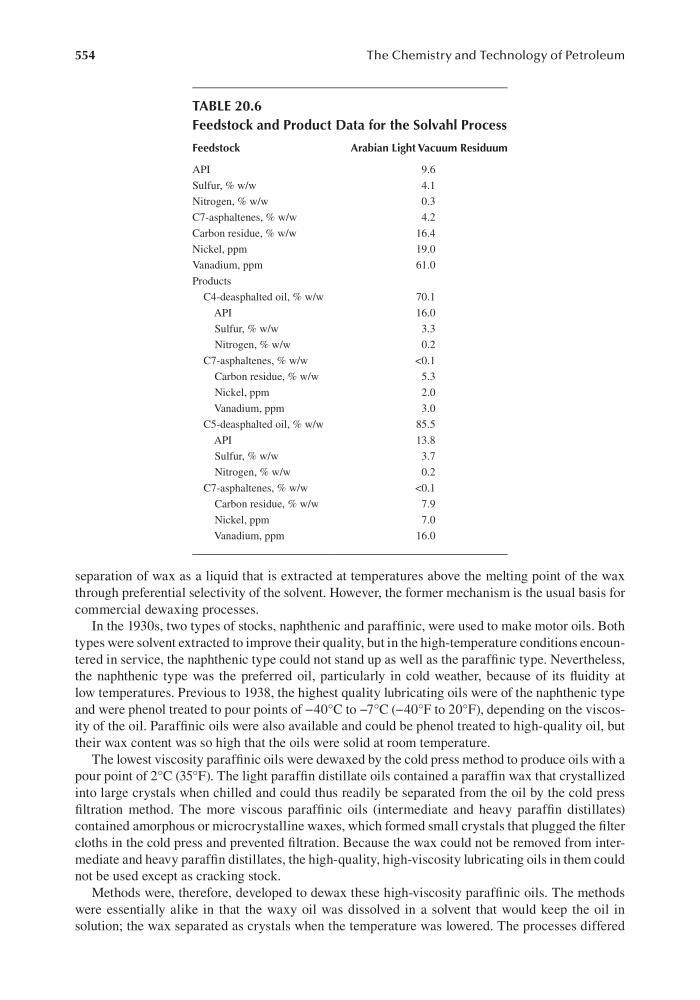
TABLE 20.6
Feedstock and Product Data for the Solvahl Process
Feedstock
Arabian Light Vacuum Residuum
API
9.6
Sulfur, % w/w
4.1
Nitrogen, % w/w
0.3
C7-asphaltenes, % w/w
4.2
Carbon residue, % w/w
16.4
Nickel, ppm
19.0
Vanadium, ppm
61.0
Products
C4-deasphalted oil, % w/w
70.1
API
16.0
Sulfur, % w/w
3.3
Nitrogen, % w/w
0.2
C7-asphaltenes, % w/w
<0.1
Carbon residue, % w/w
5.3
Nickel, ppm
2.0
Vanadium, ppm
3.0
C5-deasphalted oil, % w/w
85.5
API
13.8
Sulfur, % w/w
3.7
Nitrogen, % w/w
0.2
C7-asphaltenes, % w/w
<0.1
Carbon residue, % w/w
7.9
Nickel, ppm
7.0
Vanadium, ppm
16.0