

407
Introduction to Refining Processes
manufacture of both motor and aviation gasoline and a variation in the gas oil yield to meet changes
in the fuel oil market.
The last 40 years have seen substantial advances in the development of catalytic processes. This
has involved not only rapid advances in the chemistry and physics of the catalysts themselves but
also major engineering advances in reactor design. For example, the evolution of the design of the
catalyst beds from fixed beds to moving beds to fluidized beds. Catalyst chemistry/physics and bed
design have allowed major improvements in process efficiency and product yields.
15.6.2 modern ProCesses
Catalytic cracking is another innovation that truly belongs to the twentieth century and is regarded
as the modern method for converting high-boiling petroleum fractions, such as gas oil, into gasoline
and other low-boiling fractions. Thus, catalytic cracking in the usual commercial process involves
contacting a gas oil faction with an active catalyst under suitable conditions of temperature, pressure, and residence time so that a substantial part (>50%) of the gas oil is converted into gasoline
and lower-boiling products, usually in a single-pass operation.
However, during the cracking reaction, carbonaceous material is deposited on the catalyst, which
markedly reduces its activity, and removal of the deposit is very necessary. This is usually accomplished by burning the catalyst in the presence of air until catalyst activity is reestablished.
The several processes currently employed in catalytic cracking differ mainly in the method
of catalyst handling, although there is overlap with regard to catalyst type and the nature of the
products.
The catalyst, which may be an activated natural or synthetic material, is employed in bead, pellet,
or microspherical form and can be used as a fixed bed, moving bed, or fluid bed. The fixed-bed process was the first process to be used commercially and uses a static bed of catalyst in several reactors,
which allows a continuous flow of feedstock to be maintained. Thus, the cycle of operations consists
of (1) flow of feedstock through the catalyst bed, (2) discontinuance of feedstock flow and removal
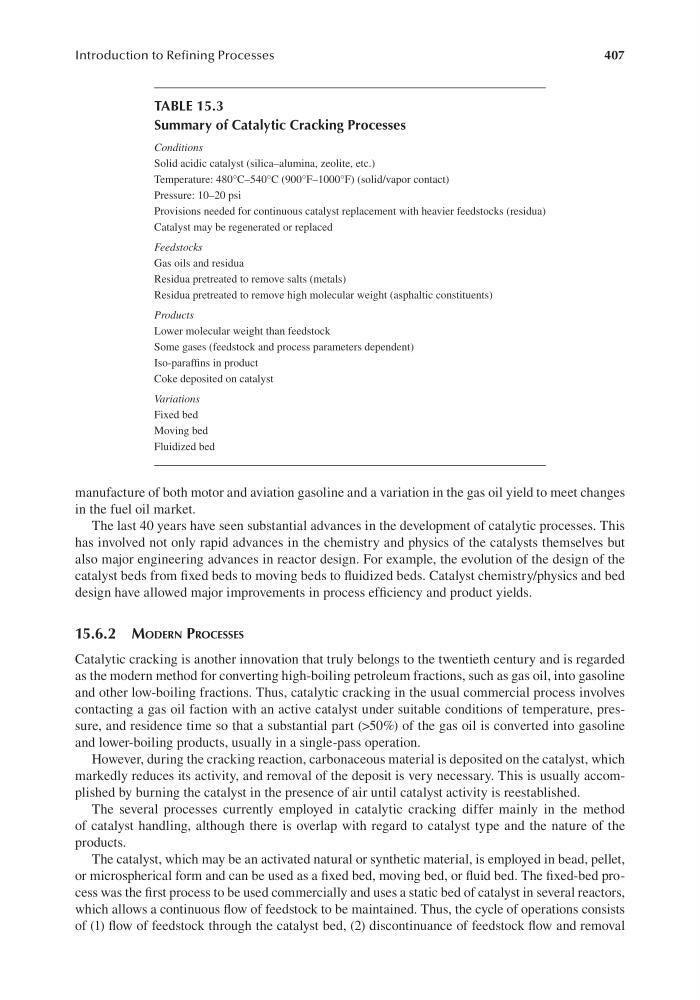
TABLE 15.3
Summary of Catalytic Cracking Processes
Conditions
Solid acidic catalyst (silica–alumina, zeolite, etc.)
Temperature: 480°C–540°C (900°F–1000°F) (solid/vapor contact)
Pressure: 10–20 psi
Provisions needed for continuous catalyst replacement with heavier feedstocks (residua)
Catalyst may be regenerated or replaced
Feedstocks
Gas oils and residua
Residua pretreated to remove salts (metals)
Residua pretreated to remove high molecular weight (asphaltic constituents)
Products
Lower molecular weight than feedstock
Some gases (feedstock and process parameters dependent)
Iso-paraffins in product
Coke deposited on catalyst
Variations
Fixed bed
Moving bed
Fluidized bed