

224
The Chemistry and Technology of Petroleum
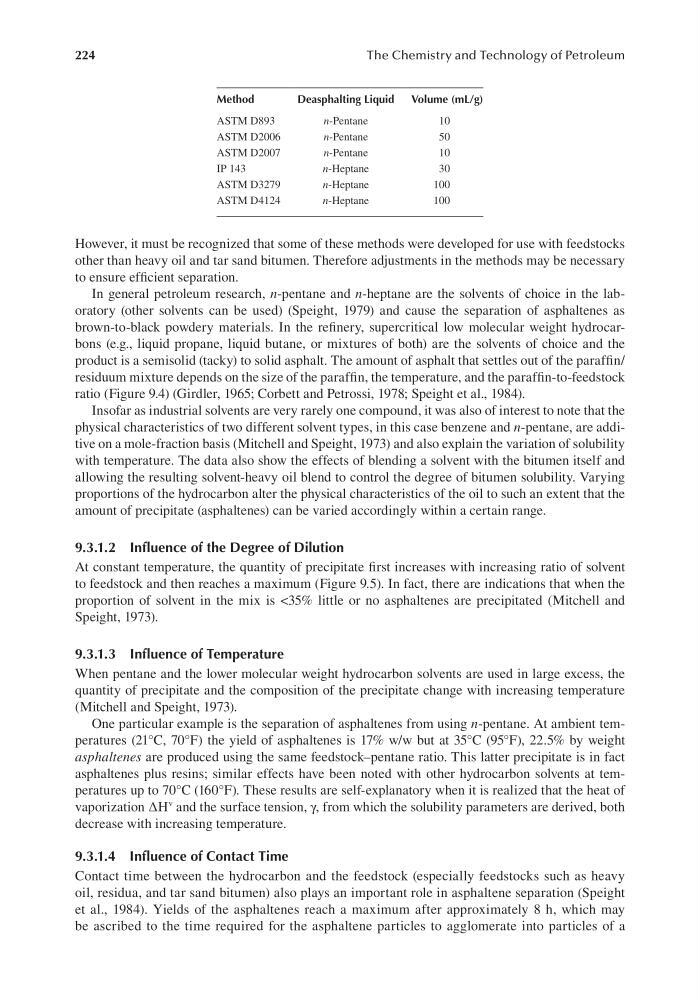
Method
Deasphalting Liquid
Volume (mL/g)
ASTM D893
n-Pentane
10
ASTM D2006
n-Pentane
50
ASTM D2007
n-Pentane
10
IP 143
n-Heptane
30
ASTM D3279
n-Heptane
100
ASTM D4124
n-Heptane
100
However, it must be recognized that some of these methods were developed for use with feedstocks
other than heavy oil and tar sand bitumen. Therefore adjustments in the methods may be necessary
to ensure efficient separation.
In general petroleum research, n-pentane and n-heptane are the solvents of choice in the laboratory (other solvents can be used) (Speight, 1979) and cause the separation of asphaltenes as
brown-to-black powdery materials. In the refinery, supercritical low molecular weight hydrocarbons (e.g., liquid propane, liquid butane, or mixtures of both) are the solvents of choice and the
product is a semisolid (tacky) to solid asphalt. The amount of asphalt that settles out of the paraffin/
residuum mixture depends on the size of the paraffin, the temperature, and the paraffin-to-feedstock
ratio (Figure 9.4) (Girdler, 1965; Corbett and Petrossi, 1978; Speight et al., 1984).
Insofar as industrial solvents are very rarely one compound, it was also of interest to note that the
physical characteristics of two different solvent types, in this case benzene and n-pentane, are additive on a mole-fraction basis (Mitchell and Speight, 1973) and also explain the variation of solubility
with temperature. The data also show the effects of blending a solvent with the bitumen itself and
allowing the resulting solvent-heavy oil blend to control the degree of bitumen solubility. Varying
proportions of the hydrocarbon alter the physical characteristics of the oil to such an extent that the
amount of precipitate (asphaltenes) can be varied accordingly within a certain range.
9.3.1.2 Influence of the Degree of Dilution
At constant temperature, the quantity of precipitate first increases with increasing ratio of solvent
to feedstock and then reaches a maximum (Figure 9.5). In fact, there are indications that when the
proportion of solvent in the mix is <35% little or no asphaltenes are precipitated (Mitchell and
Speight, 1973).
9.3.1.3 Influence of Temperature
When pentane and the lower molecular weight hydrocarbon solvents are used in large excess, the
quantity of precipitate and the composition of the precipitate change with increasing temperature
(Mitchell and Speight, 1973).
One particular example is the separation of asphaltenes from using n-pentane. At ambient temperatures (21°C, 70°F) the yield of asphaltenes is 17% w/w but at 35°C (95°F), 22.5% by weight
asphaltenes are produced using the same feedstock–pentane ratio. This latter precipitate is in fact
asphaltenes plus resins; similar effects have been noted with other hydrocarbon solvents at temperatures up to 70°C (160°F). These results are self-explanatory when it is realized that the heat of
vaporization ∆H
v
and the surface tension, γ, from which the solubility parameters are derived, both
decrease with increasing temperature.
9.3.1.4 Influence of Contact Time
Contact time between the hydrocarbon and the feedstock (especially feedstocks such as heavy
oil, residua, and tar sand bitumen) also plays an important role in asphaltene separation (Speight
et al., 1984). Yields of the asphaltenes reach a maximum after approximately 8 h, which may
be ascribed to the time required for the asphaltene particles to agglomerate into particles of a