

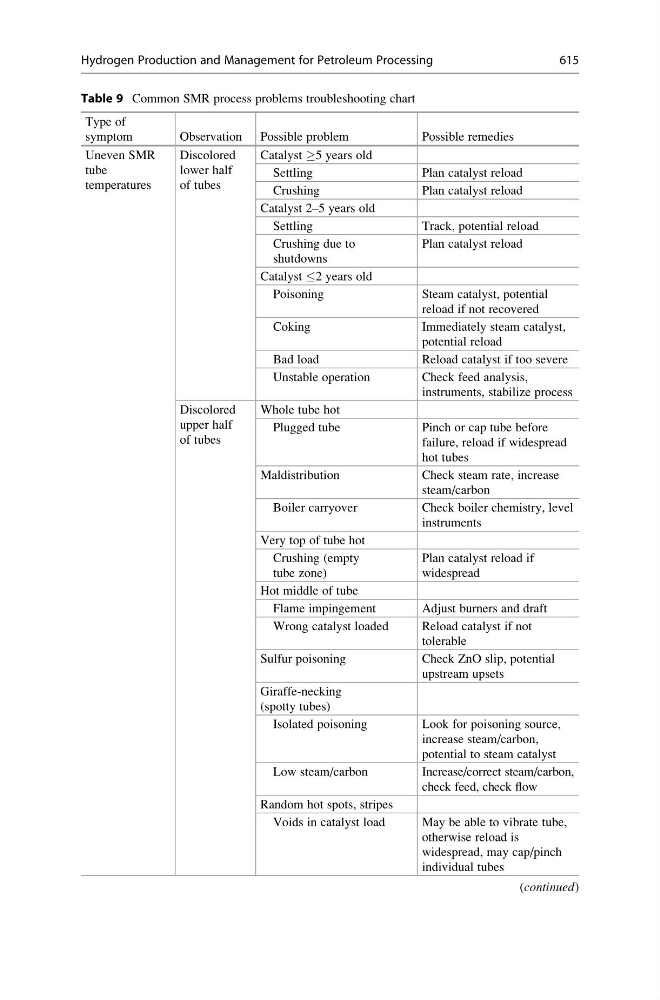
Table 9 Common SMR process problems troubleshooting chart
Type of
symptom
Observation Possible problem
Possible remedies
Uneven SMR
tube
temperatures
Discolored
lower half
of tubes
Catalyst !5 years old
Settling
Plan catalyst reload
Crushing
Plan catalyst reload
Catalyst 2–5 years old
Settling
Track, potential reload
Crushing due to
shutdowns
Plan catalyst reload
Catalyst 2 years old
Poisoning
Steam catalyst, potential
reload if not recovered
Coking
Immediately steam catalyst,
potential reload
Bad load
Reload catalyst if too severe
Unstable operation
Check feed analysis,
instruments, stabilize process
Discolored
upper half
of tubes
Whole tube hot
Plugged tube
Pinch or cap tube before
failure, reload if widespread
hot tubes
Maldistribution
Check steam rate, increase
steam/carbon
Boiler carryover
Check boiler chemistry, level
instruments
Very top of tube hot
Crushing (empty
tube zone)
Plan catalyst reload if
widespread
Hot middle of tube
Flame impingement
Adjust burners and draft
Wrong catalyst loaded
Reload catalyst if not
tolerable
Sulfur poisoning
Check ZnO slip, potential
upstream upsets
Giraffe-necking
(spotty tubes)
Isolated poisoning
Look for poisoning source,
increase steam/carbon,
potential to steam catalyst
Low steam/carbon
Increase/correct steam/carbon,
check feed, check flow
Random hot spots, stripes
Voids in catalyst load
May be able to vibrate tube,
otherwise reload is
widespread, may cap/pinch
individual tubes
(continued)
Hydrogen Production and Management for Petroleum Processing
615