

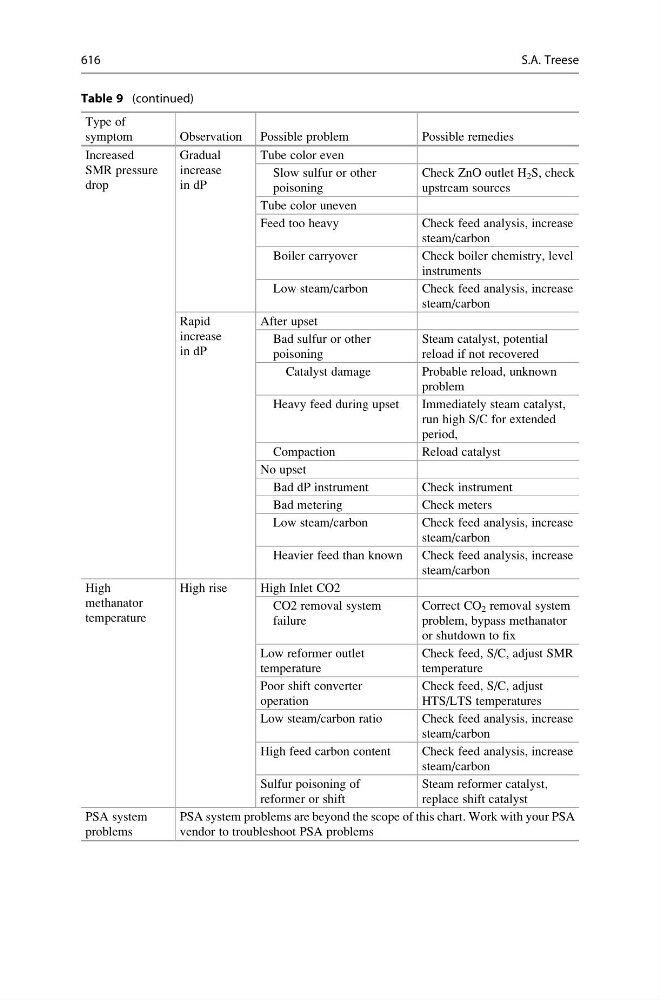
Table 9 (continued)
Type of
symptom
Observation Possible problem
Possible remedies
Increased
SMR pressure
drop
Gradual
increase
in dP
Tube color even
Slow sulfur or other
poisoning
Check ZnO outlet H 2 S, check
upstream sources
Tube color uneven
Feed too heavy
Check feed analysis, increase
steam/carbon
Boiler carryover
Check boiler chemistry, level
instruments
Low steam/carbon
Check feed analysis, increase
steam/carbon
Rapid
increase
in dP
After upset
Bad sulfur or other
poisoning
Steam catalyst, potential
reload if not recovered
Catalyst damage
Probable reload, unknown
problem
Heavy feed during upset
Immediately steam catalyst,
run high S/C for extended
period,
Compaction
Reload catalyst
No upset
Bad dP instrument
Check instrument
Bad metering
Check meters
Low steam/carbon
Check feed analysis, increase
steam/carbon
Heavier feed than known
Check feed analysis, increase
steam/carbon
High
methanator
temperature
High rise
High Inlet CO2
CO2 removal system
failure
Correct CO 2 removal system
problem, bypass methanator
or shutdown to fix
Low reformer outlet
temperature
Check feed, S/C, adjust SMR
temperature
Poor shift converter
operation
Check feed, S/C, adjust
HTS/LTS temperatures
Low steam/carbon ratio
Check feed analysis, increase
steam/carbon
High feed carbon content
Check feed analysis, increase
steam/carbon
Sulfur poisoning of
reformer or shift
Steam reformer catalyst,
replace shift catalyst
PSA system
problems
PSA system problems are beyond the scope of this chart. Work with your PSA
vendor to troubleshoot PSA problems
616
S.A. Treese