

48
J. Karloopia et al.
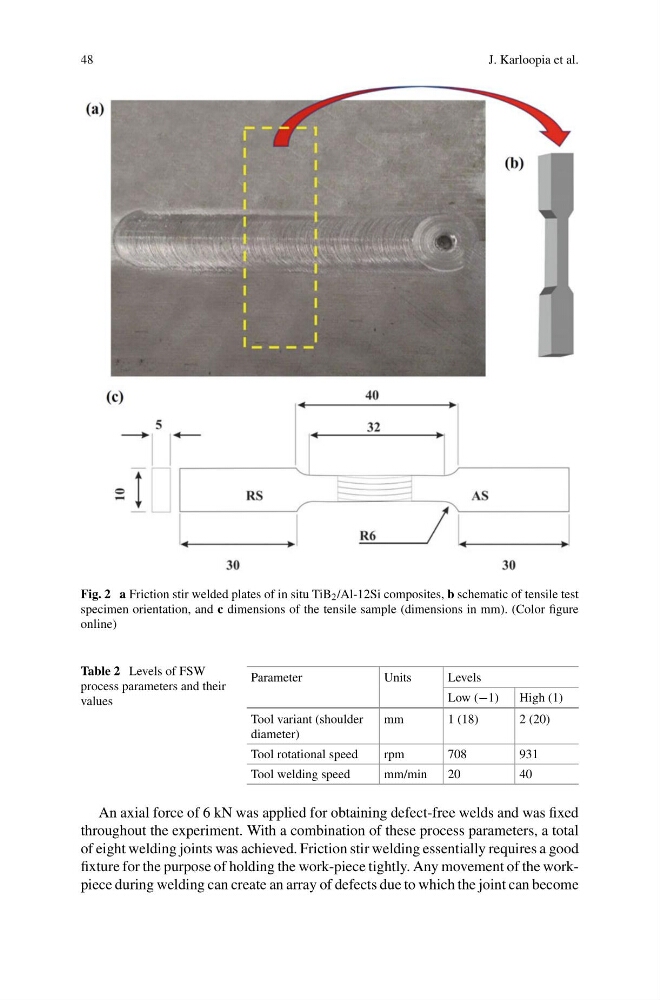
Fig. 2 a Friction stir welded plates of in situ TiB 2 /Al-12Si composites, b schematic of tensile test
specimen orientation, and c dimensions of the tensile sample (dimensions in mm). (Color figure
online)
Table 2 Levels of FSW
process parameters and their
values
Parameter
Units
Levels
Low (−1)
High (1)
Tool variant (shoulder
diameter)
mm
1 (18)
2 (20)
Tool rotational speed
rpm
708
931
Tool welding speed
mm/min
20
40
An axial force of 6 kN was applied for obtaining defect-free welds and was fixed
throughout the experiment. With a combination of these process parameters, a total
of eight welding joints was achieved. Friction stir welding essentially requires a good
fixture for the purpose of holding the work-piece tightly. Any movement of the workpiece during welding can create an array of defects due to which the joint can become