

338
M. Rasinac et al.
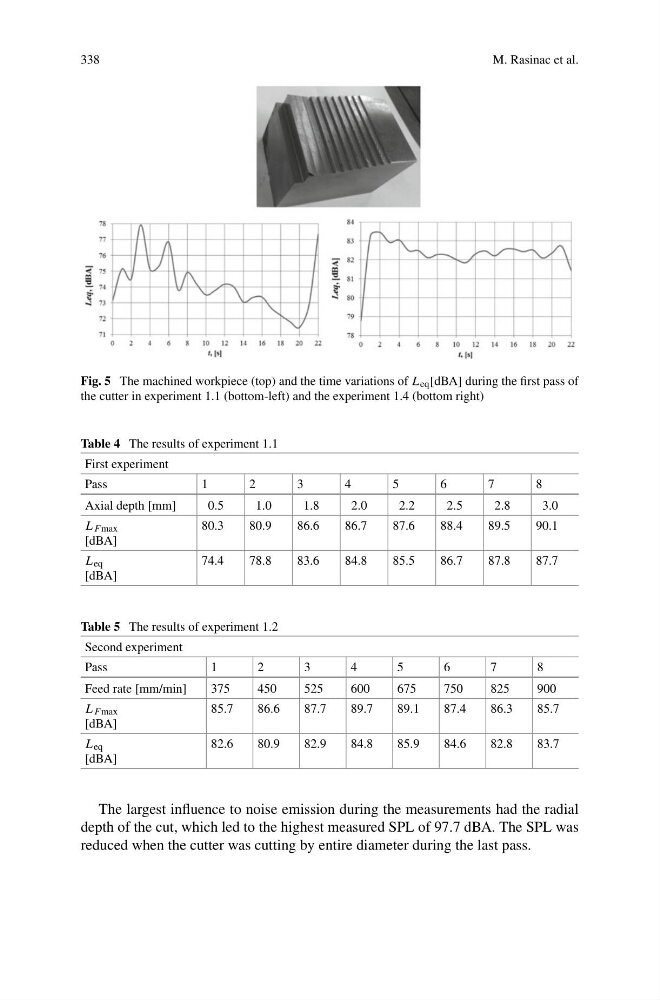
Fig. 5 The machined workpiece (top) and the time variations of L eq [dBA] during the first pass of
the cutter in experiment 1.1 (bottom-left) and the experiment 1.4 (bottom right)
Table 4 The results of experiment 1.1
First experiment
Pass
1
2
3
4
5
6
7
8
Axial depth [mm]
0.5
1.0
1.8
2.0
2.2
2.5
2.8
3.0
L Fmax
[dBA]
80.3
80.9
86.6
86.7
87.6
88.4
89.5
90.1
L eq
[dBA]
74.4
78.8
83.6
84.8
85.5
86.7
87.8
87.7
Table 5 The results of experiment 1.2
Second experiment
Pass
1
2
3
4
5
6
7
8
Feed rate [mm/min]
375
450
525
600
675
750
825
900
L Fmax
[dBA]
85.7
86.6
87.7
89.7
89.1
87.4
86.3
85.7
L eq
[dBA]
82.6
80.9
82.9
84.8
85.9
84.6
82.8
83.7
The largest influence to noise emission during the measurements had the radial
depth of the cut, which led to the highest measured SPL of 97.7 dBA. The SPL was
reduced when the cutter was cutting by entire diameter during the last pass.