

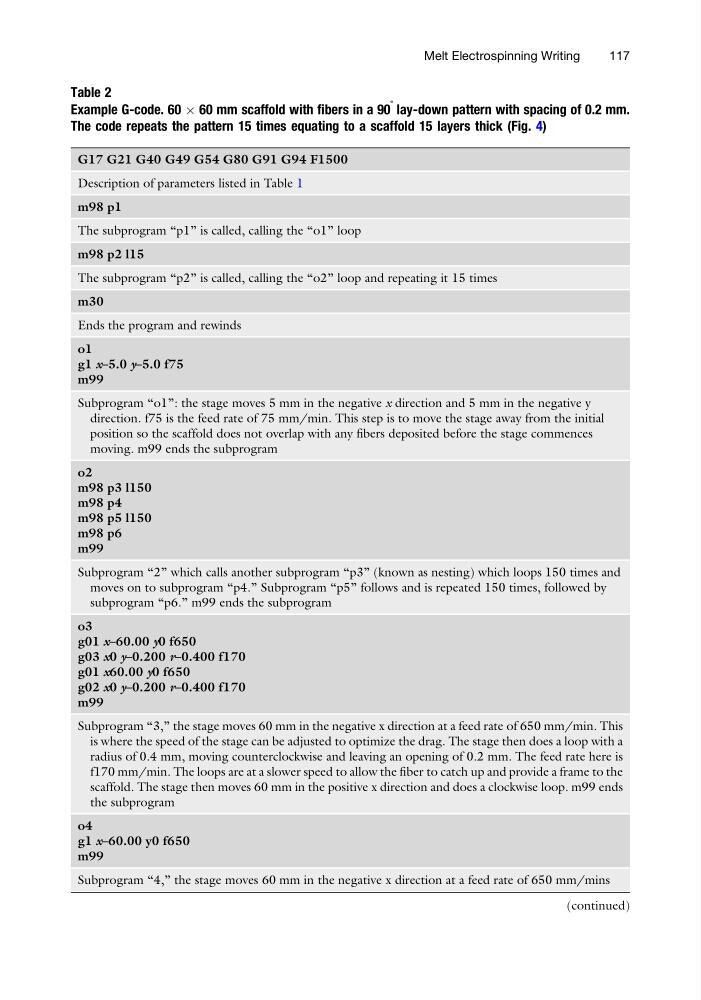
Table 2
Example G-code. 60 Â 60 mm scaffold with fibers in a 90
˚ lay-down pattern with spacing of 0.2 mm.
The code repeats the pattern 15 times equating to a scaffold 15 layers thick (Fig. 4)
G17 G21 G40 G49 G54 G80 G91 G94 F1500
Description of parameters listed in Table 1
m98 p1
The subprogram “p1” is called, calling the “o1” loop
m98 p2 l15
The subprogram “p2” is called, calling the “o2” loop and repeating it 15 times
m30
Ends the program and rewinds
o1
g1 x–5.0 y–5.0 f75
m99
Subprogram “o1”: the stage moves 5 mm in the negative x direction and 5 mm in the negative y
direction. f75 is the feed rate of 75 mm/min. This step is to move the stage away from the initial
position so the scaffold does not overlap with any fibers deposited before the stage commences
moving. m99 ends the subprogram
o2
m98 p3 l150
m98 p4
m98 p5 l150
m98 p6
m99
Subprogram “2” which calls another subprogram “p3” (known as nesting) which loops 150 times and
moves on to subprogram “p4.” Subprogram “p5” follows and is repeated 150 times, followed by
subprogram “p6.” m99 ends the subprogram
o3
g01 x–60.00 y0 f650
g03 x0 y–0.200 r–0.400 f170
g01 x60.00 y0 f650
g02 x0 y–0.200 r–0.400 f170
m99
Subprogram “3,” the stage moves 60 mm in the negative x direction at a feed rate of 650 mm/min. This
is where the speed of the stage can be adjusted to optimize the drag. The stage then does a loop with a
radius of 0.4 mm, moving counterclockwise and leaving an opening of 0.2 mm. The feed rate here is
f170 mm/min. The loops are at a slower speed to allow the fiber to catch up and provide a frame to the
scaffold. The stage then moves 60 mm in the positive x direction and does a clockwise loop. m99 ends
the subprogram
o4
g1 x–60.00 y0 f650
m99
Subprogram “4,” the stage moves 60 mm in the negative x direction at a feed rate of 650 mm/mins
(continued)
Melt Electrospinning Writing
117