

10 A Novel High-Efficiency Keyhole Tungsten Inert Gas …
331
where K q =
h
L +2
3
, ϕ 1 + ϕ 2 = 1. They are energy distribution coefficients; arc
voltage is represented as U ; thermal efficiency is represented as ηwelding current is
represented as I . σ i and σ k are heat distribution parameters; the changing height of
the keyhole is represented as h, and r 1 stands for the arc radius.
10.3 Signal Characteristics in K-TIG Welding
Keyhole Tungsten Inert Gas welding is a much complex physical process, during
which the thermal field, optical field, acoustic field, force filed, magnetic field and
electrical field are coupling with each other. There is a certain relation between
different physical phenomena, indicating the real-time welding quality somehow.
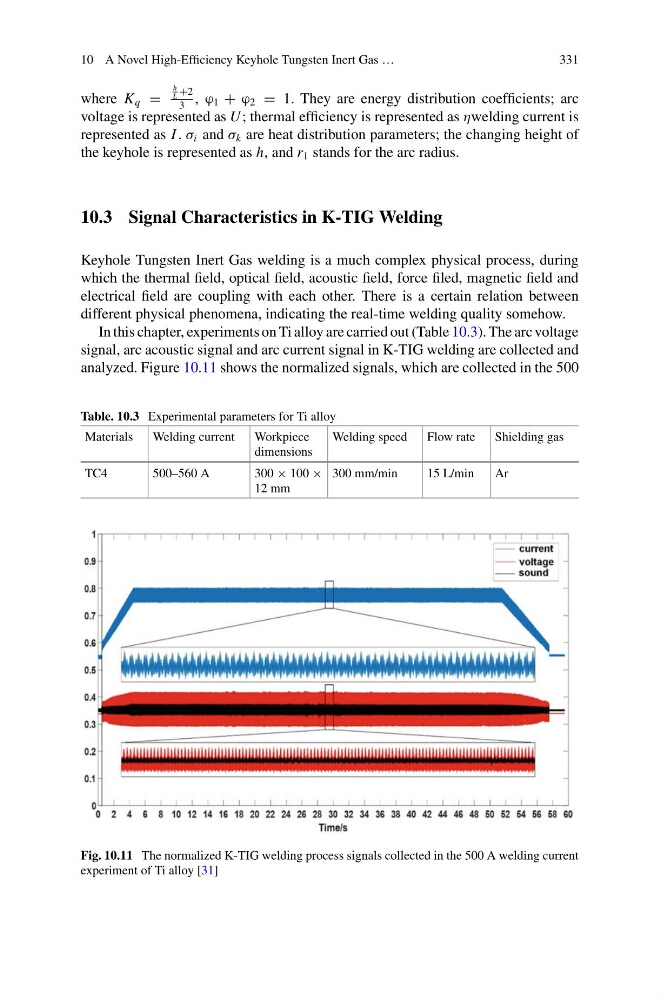
In this chapter, experiments on Ti alloy are carried out (Table 10.3). The arc voltage
signal, arc acoustic signal and arc current signal in K-TIG welding are collected and
analyzed. Figure 10.11 shows the normalized signals, which are collected in the 500
Table. 10.3 Experimental parameters for Ti alloy
Materials
Welding current
Workpiece
dimensions
Welding speed
Flow rate
Shielding gas
TC4
500–560 A
300 × 100 ×
12 mm
300 mm/min
15 L/min
Ar
Fig. 10.11 The normalized K-TIG welding process signals collected in the 500 A welding current
experiment of Ti alloy [31]