

Automated Upgraded Generalized Full-Discretization Method …
97
1
1.1
1.2
1.3
spindle speed [rpm]
10
4
6
8
10
12
14
16
depth of cut [mm]
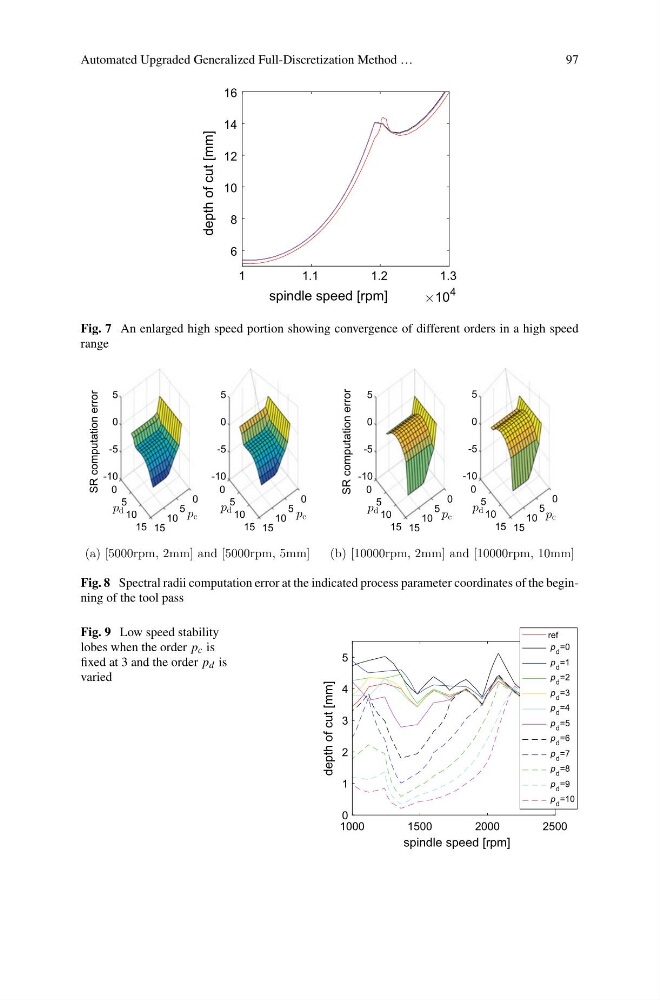
Fig. 7 An enlarged high speed portion showing convergence of different orders in a high speed
range
0
p c
5
10
15
15
10
5
p d
SR computation error
-10
-5
0
5
0
p c
0
5
10
15
15
10
5
p d
5
0
-5
-10
0
(a) [5000rpm, 2mm] and [5000rpm, 5mm]
0
p c
5
10
15
15
10
5
p d
5
-10
0
-5
0
SR computation error
0
p c
5
10
15
15
10
5
p d
0
5
-5
-10
0
(b) [10000rpm, 2mm] and [10000rpm, 10mm]
Fig. 8 Spectral radii computation error at the indicated process parameter coordinates of the beginning of the tool pass
Fig. 9 Low speed stability
lobes when the order p c is
fixed at 3 and the order p d is
varied
1000
1500
2000
2500
spindle speed [rpm]
0
1
2
3
4
5
depth of cut [mm]
ref
p d =0
p d =1
p d =2
p d =3
p d =4
p d =5
p d =6
p d =7
p d =8
p d =9
p d =10