

7 Micro-hole Arrays and Net-like Structure Fabrication …
217
laser action time and the laser power density. When the laser irradiation intensity
is much higher than the ablation threshold, the strong ablation process is dominant.
When the laser irradiation intensity is near the ablation threshold, the weak cupping
process caused by Coulomb explosion is dominant. At the same time, however, the
ablation threshold and single-pulse ablation depth of the material are directly related
to the properties of the material itself, the laser irradiation intensity, and the number
of laser pulses.
7.3 Fabricating Micro-hole Arrays on Fused Silica Sheet
7.3.1 Overview of Laser Micro-holes Machining Technology
In fact, each micro-hole precision machining methods have their own advantages
and disadvantages. Among them, the mechanical drilling is more common way of
processing micro-pores, but it is not widely used in the field of micro-processing.
Mechanical drilling needs to rely on drilling tools and other bits, which limit the
range of processed materials. While the size of the drill bit and the rigidity of the drill
limited the size of the holes made by mechanical processing, the general diameter of
micro-holes can only be greater than 30 μm, and depth-to-diameter ratio is generally
less than 5 μm. However, due to the micro-holes in the micron or even nanometer
order often bring great difficulties to the manufacturing process. At present, there are
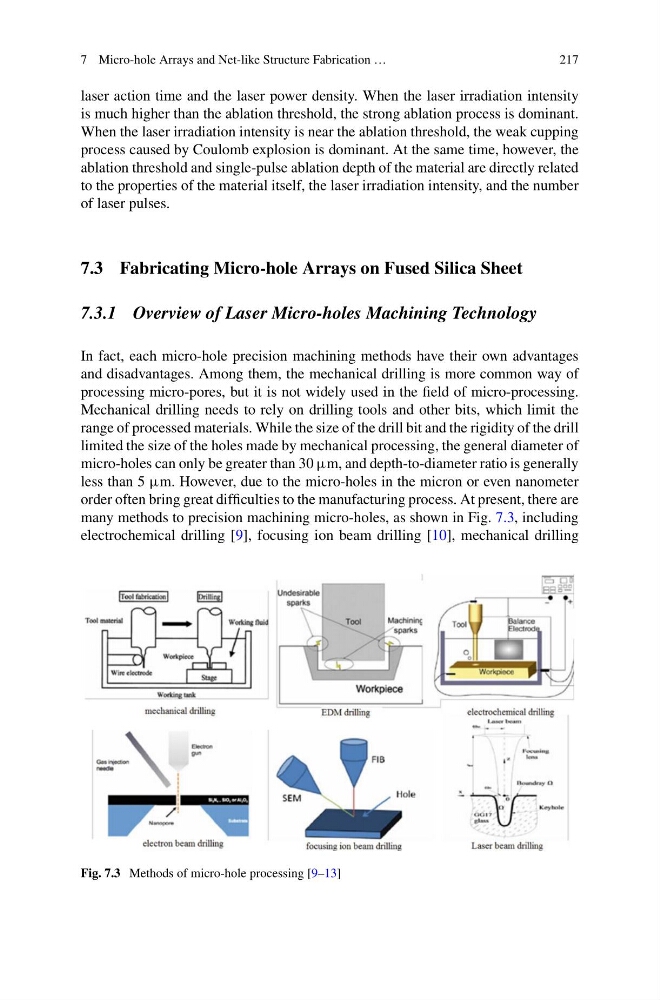
many methods to precision machining micro-holes, as shown in Fig. 7.3, including
electrochemical drilling [9], focusing ion beam drilling [10], mechanical drilling
Fig. 7.3 Methods of micro-hole processing [9–13]