

2 ISOALKY ™ Technology: Next-Generation Alkylate Gasoline …
41
In conventional alkylation plants, rapid buildup of conjunct polymer in an acid
catalyst may occur in case of a severe unit upset. In this case, the acid catalyst with
high-conjunct polymer may form an inseparable emulsion with the hydrocarbon, and
a massive amount of acidic emulsion can be carried to the distillation section causing
plant downtime and equipment corrosion. This situation is called acid runaway [20].
Conventional alkylation processes are carefully controlled to prevent this situation
from occurring.
The ISOALKY Technology has no risk of acid runaway due to the low volume of
the ionic liquid catalyst in the process and the limited solubility of hydrocarbon in
the ionic liquid catalyst. Impacts of severe process upsets and continuous buildup of
conjunct polymer in the ionic liquid were alleviated by reducing the olefin feed and
continuing on-line regeneration of the ionic liquid catalyst.
2.7 ISOALKY Technology Sub-processes and Key Features
2.7.1 Alkylation Reactor
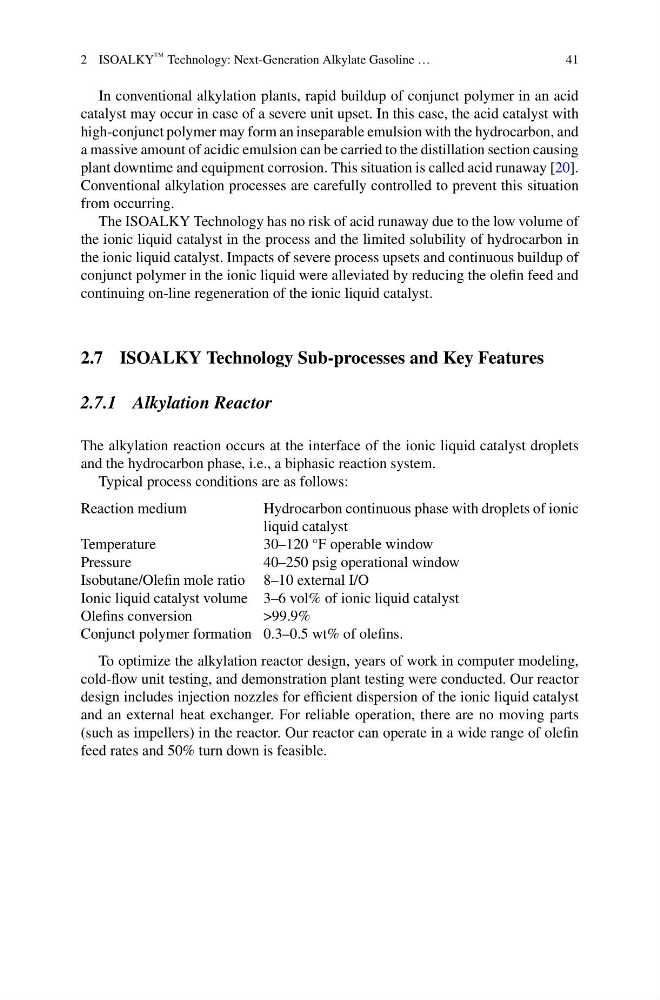
The alkylation reaction occurs at the interface of the ionic liquid catalyst droplets
and the hydrocarbon phase, i.e., a biphasic reaction system.
Typical process conditions are as follows:
Reaction medium
Hydrocarbon continuous phase with droplets of ionic
liquid catalyst
Temperature
30–120 °F operable window
Pressure
40–250 psig operational window
Isobutane/Olefin mole ratio 8–10 external I/O
Ionic liquid catalyst volume 3–6 vol% of ionic liquid catalyst
Olefins conversion
>99.9%
Conjunct polymer formation 0.3–0.5 wt% of olefins.
To optimize the alkylation reactor design, years of work in computer modeling,
cold-flow unit testing, and demonstration plant testing were conducted. Our reactor
design includes injection nozzles for efficient dispersion of the ionic liquid catalyst
and an external heat exchanger. For reliable operation, there are no moving parts
(such as impellers) in the reactor. Our reactor can operate in a wide range of olefin
feed rates and 50% turn down is feasible.