

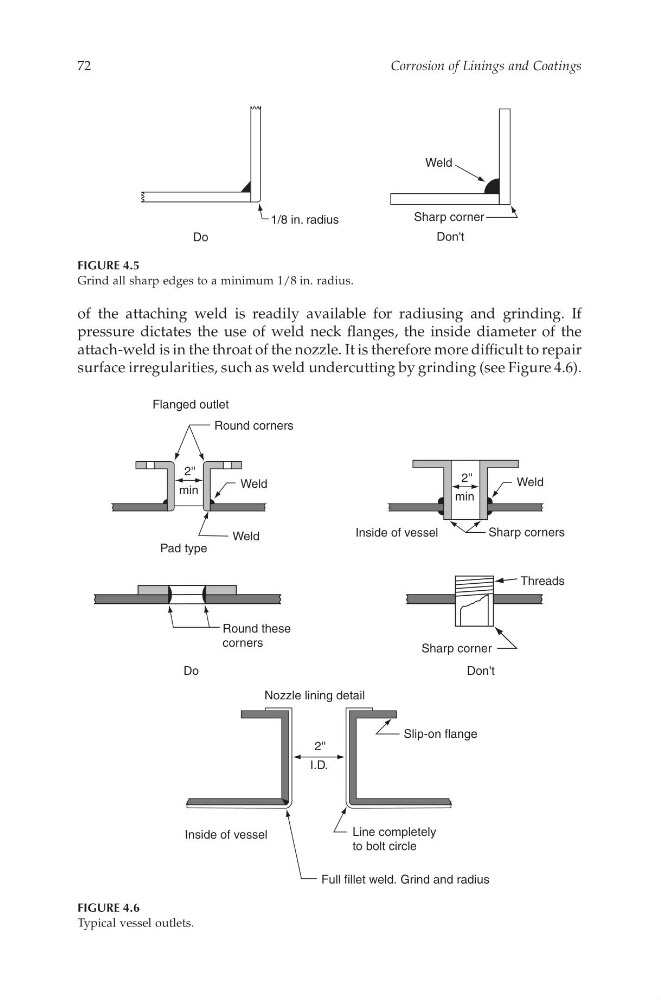
of the attaching weld is readily available for radiusing and grinding. If
pressured ictates the use of weld neck flanges, the inside diameter of the
attach-weldisinthe throat of the nozzle. It is thereforemore difficult to repair
surfaceirregularities, suchasweld undercutting by grinding (seeFigure 4.6).
Do
Don't
Weld
Sharpcorner
1/8 in. radius
FIGURE 4.5
Grind all sharp edges to aminimum 1/8 in. radius.
Weld
Weld
Padtype
Round these
corners
Round corners
Flanged outlet
2''
min
2''
I.D.
2''
min
Weld
Sharpcorners
Inside of vessel
Inside of vessel
Threads
Sharpcorner
Do
Don't
Slip-on flange
Line completely
to bolt circle
Full fillet weld. Grind and radius
Nozzle lining detail
FIGURE 4.6
Typical vessel outlets.
Corrosion of Linings and Coatings
72
CAT8247—CHAPTER 4—17/10/2006—14:33—SRIDHAR—XML MODEL B–pp. 69–174