

If possible, avoid the use of bolted joints. Should it be necessary to use
ab olted joint,i ts hould be of corrosion-resistant materials and sealed shut.
The mating surfaceofsteel surfaces should be gasketed. The lining material
should be applied prior to bolting.
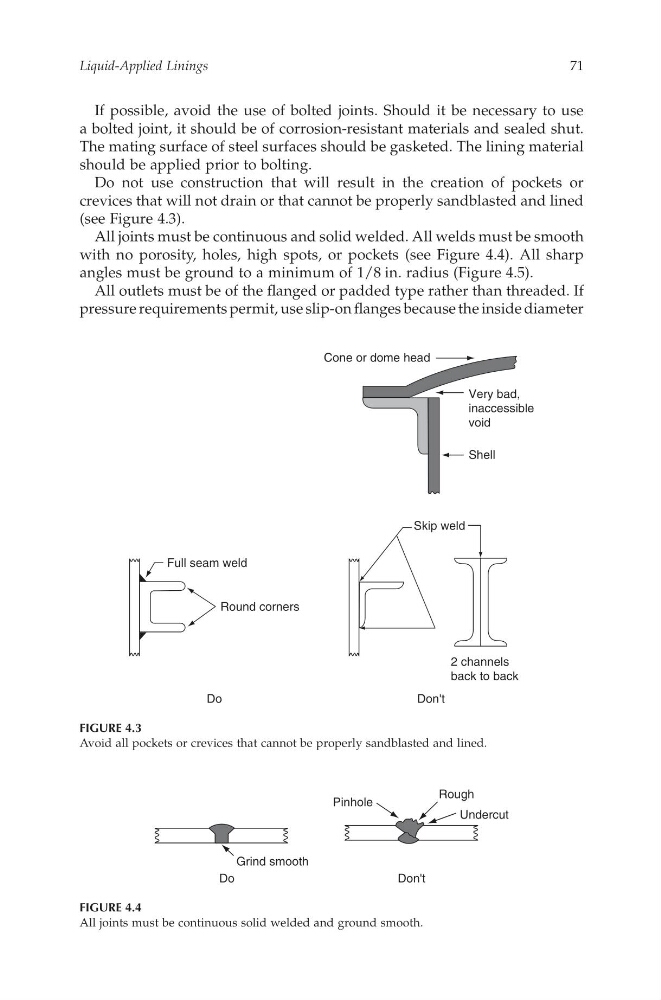
Do not use constructiont hat willr esult in the creation of pockets or
crevices that will not drain or that cannot be properly sandblasted and lined
(see Figure 4.3).
All jointsmust be continuous and solid welded. All welds must be smooth
with no porosity,h oles, high spots, or pockets (seeF igure 4.4). All sharp
anglesm ust be ground to am inimumof1 /8 in. radius( Figure 4.5).
All outlets must be of the flangedorpadded type rather than threaded. If
pressurerequirements permit, use slip-on flanges because the inside diameter
Cone or dome head
Very bad,
inaccessible
void
Shell
Skip weld
2channels
back to back
Full seam weld
Round corners
Do
Don't
FIGURE 4.3
Avoid all pockets or crevices that cannot be properly sandblasted and lined.
Do
Don't
Grind smooth
Pinhole
Rough
Undercut
FIGURE 4.4
All joints must be continuous solid welded and ground smooth.
Liquid-Applied Linings
71
CAT8247—CHAPTER 4—17/10/2006—14:33—SRIDHAR—XML MODEL B–pp. 69–174