

3 Design of Household Appliances Considering Remanufacturing …
39
Table 3.3 (continued)
Influence factor Failure factor
Criteria for determining
improvement strategy
Improvement strategy
Convenience of
fastening and
disassembling
Difficulty in fastening
and disassembling
In case of
non-destructive cracking
method using adhesive
or welding, it is possible
to change by bolt or
snap fit method
• Changed to fastening
method that can be
used for
non-destructive
disassembly
Extraction and
Insert ability
Access to coupling
elements is inefficient
If it is difficult to
visually identify the
fastening position
• Valid marks
Tool accessibility Inefficient accessibility If the depth of the screw
hole is too deep
• Injection structure
change such as
embossing of joint
part
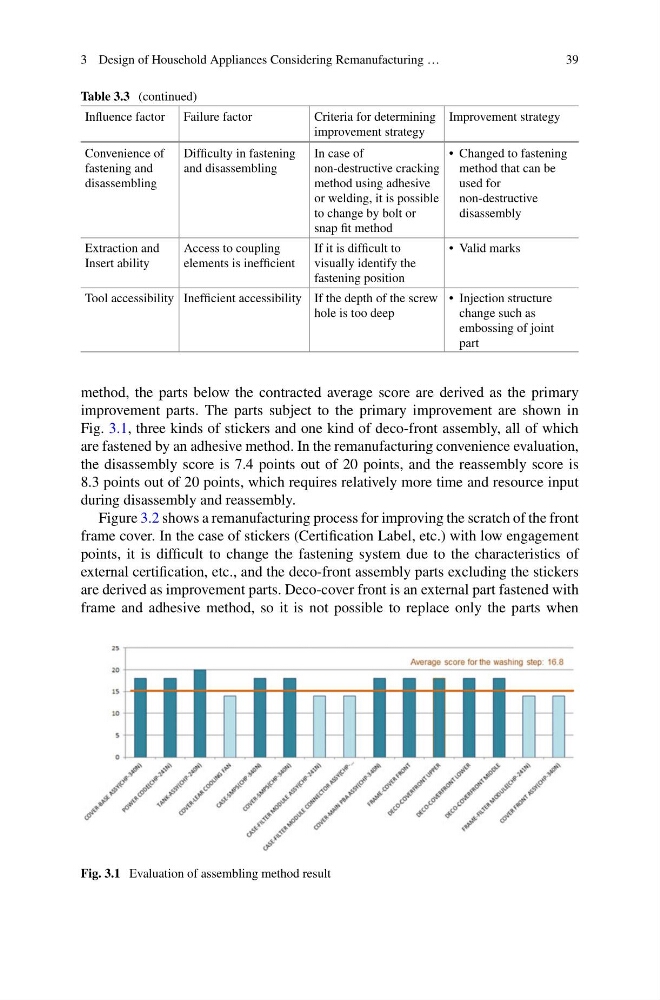
method, the parts below the contracted average score are derived as the primary
improvement parts. The parts subject to the primary improvement are shown in
Fig. 3.1, three kinds of stickers and one kind of deco-front assembly, all of which
are fastened by an adhesive method. In the remanufacturing convenience evaluation,
the disassembly score is 7.4 points out of 20 points, and the reassembly score is
8.3 points out of 20 points, which requires relatively more time and resource input
during disassembly and reassembly.
Figure 3.2 shows a remanufacturing process for improving the scratch of the front
frame cover. In the case of stickers (Certification Label, etc.) with low engagement
points, it is difficult to change the fastening system due to the characteristics of
external certification, etc., and the deco-front assembly parts excluding the stickers
are derived as improvement parts. Deco-cover front is an external part fastened with
frame and adhesive method, so it is not possible to replace only the parts when
Fig. 3.1 Evaluation of assembling method result