

40
H.-Y. Kang et al.
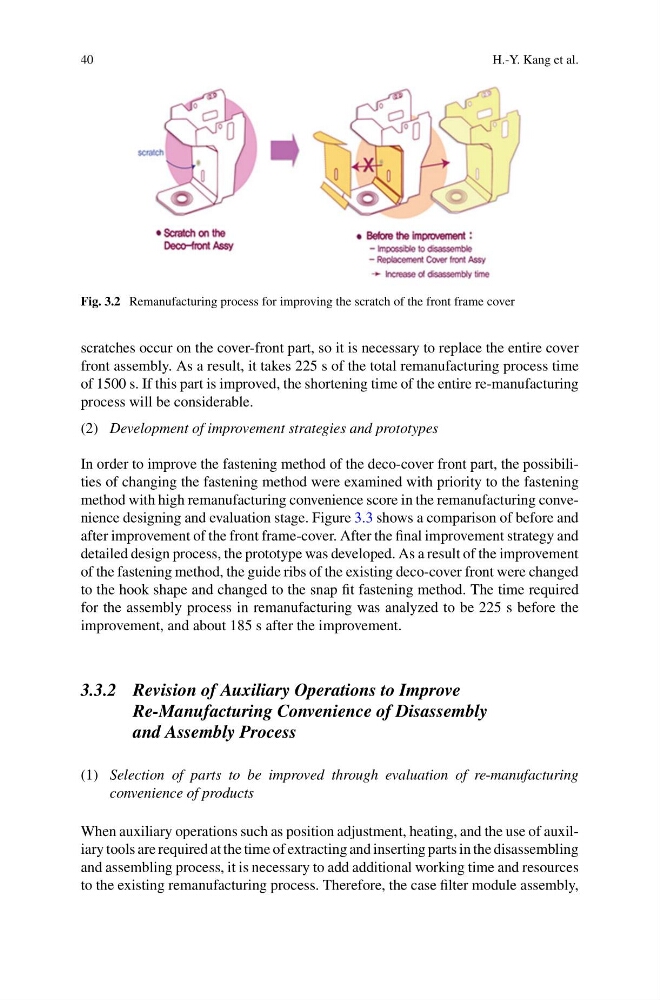
Fig. 3.2 Remanufacturing process for improving the scratch of the front frame cover
scratches occur on the cover-front part, so it is necessary to replace the entire cover
front assembly. As a result, it takes 225 s of the total remanufacturing process time
of 1500 s. If this part is improved, the shortening time of the entire re-manufacturing
process will be considerable.
(2) Development of improvement strategies and prototypes
In order to improve the fastening method of the deco-cover front part, the possibilities of changing the fastening method were examined with priority to the fastening
method with high remanufacturing convenience score in the remanufacturing convenience designing and evaluation stage. Figure 3.3 shows a comparison of before and
after improvement of the front frame-cover. After the final improvement strategy and
detailed design process, the prototype was developed. As a result of the improvement
of the fastening method, the guide ribs of the existing deco-cover front were changed
to the hook shape and changed to the snap fit fastening method. The time required
for the assembly process in remanufacturing was analyzed to be 225 s before the
improvement, and about 185 s after the improvement.
3.3.2 Revision of Auxiliary Operations to Improve
Re-Manufacturing Convenience of Disassembly
and Assembly Process
(1) Selection of parts to be improved through evaluation of re-manufacturing
convenience of products
When auxiliary operations such as position adjustment, heating, and the use of auxiliary tools are required at the time of extracting and inserting parts in the disassembling
and assembling process, it is necessary to add additional working time and resources
to the existing remanufacturing process. Therefore, the case filter module assembly,