

228
H. H. Jadav et al.
Fig. 5 BTFSW surface appearance for Al-Al (a, b, d) top surface (c) and (e) bottom surface
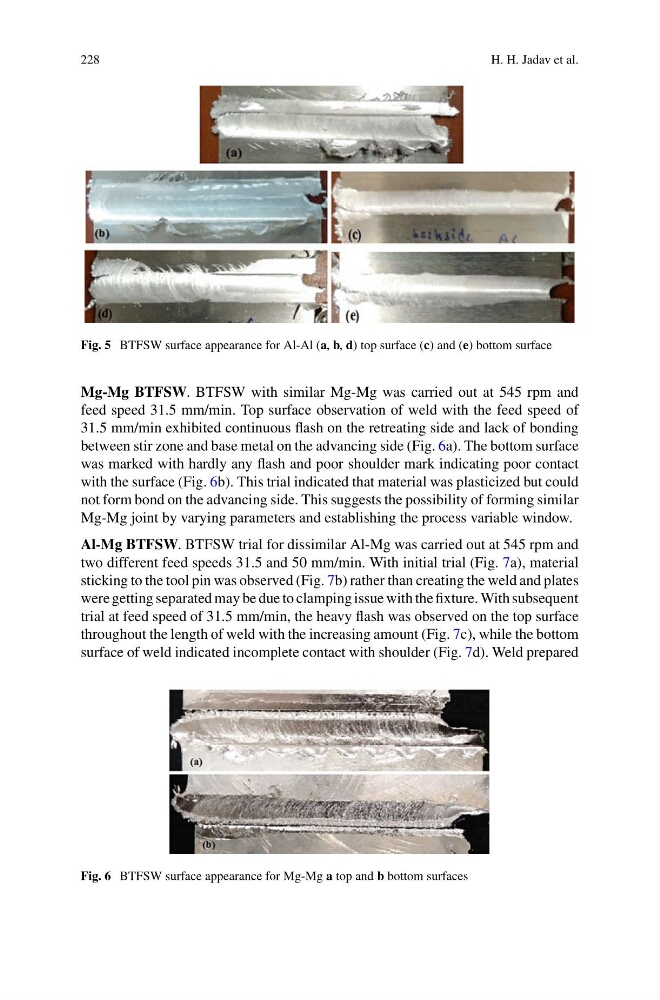
Mg-Mg BTFSW. BTFSW with similar Mg-Mg was carried out at 545 rpm and
feed speed 31.5 mm/min. Top surface observation of weld with the feed speed of
31.5 mm/min exhibited continuous flash on the retreating side and lack of bonding
between stir zone and base metal on the advancing side (Fig. 6a). The bottom surface
was marked with hardly any flash and poor shoulder mark indicating poor contact
with the surface (Fig. 6b). This trial indicated that material was plasticized but could
not form bond on the advancing side. This suggests the possibility of forming similar
Mg-Mg joint by varying parameters and establishing the process variable window.
Al-Mg BTFSW. BTFSW trial for dissimilar Al-Mg was carried out at 545 rpm and
two different feed speeds 31.5 and 50 mm/min. With initial trial (Fig. 7a), material
sticking to the tool pin was observed (Fig. 7b) rather than creating the weld and plates
were getting separated may be due to clamping issue with the fixture. With subsequent
trial at feed speed of 31.5 mm/min, the heavy flash was observed on the top surface
throughout the length of weld with the increasing amount (Fig. 7c), while the bottom
surface of weld indicated incomplete contact with shoulder (Fig. 7d). Weld prepared
Fig. 6 BTFSW surface appearance for Mg-Mg a top and b bottom surfaces