

Applicability of Bobbin Tool Friction Stir Welding …
227
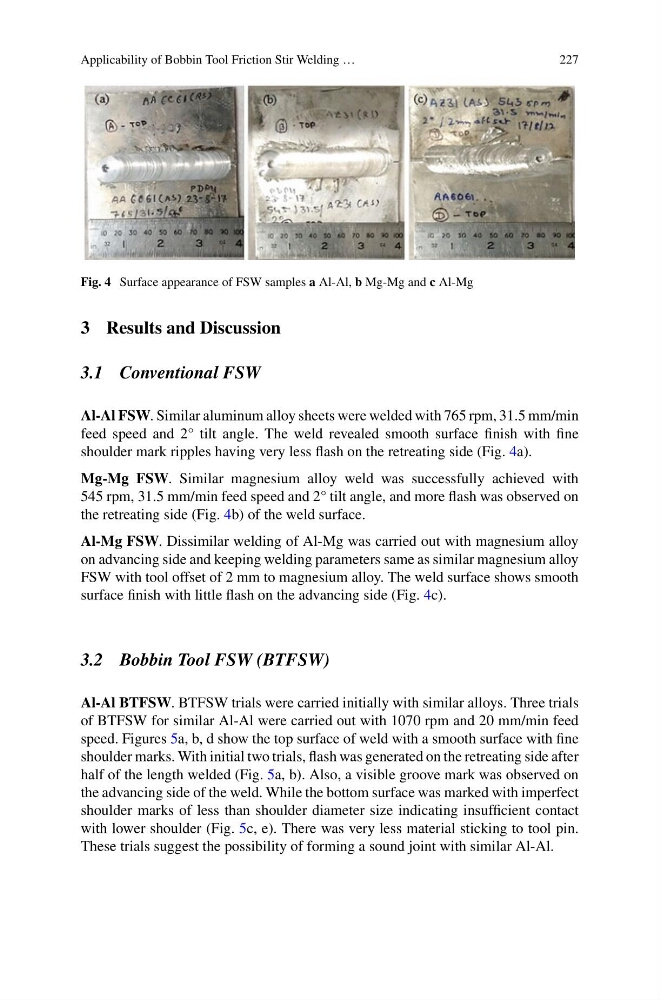
Fig. 4 Surface appearance of FSW samples a Al-Al, b Mg-Mg and c Al-Mg
3 Results and Discussion
3.1 Conventional FSW
Al-Al FSW. Similar aluminum alloy sheets were welded with 765 rpm, 31.5 mm/min
feed speed and 2° tilt angle. The weld revealed smooth surface finish with fine
shoulder mark ripples having very less flash on the retreating side (Fig. 4a).
Mg-Mg FSW. Similar magnesium alloy weld was successfully achieved with
545 rpm, 31.5 mm/min feed speed and 2° tilt angle, and more flash was observed on
the retreating side (Fig. 4b) of the weld surface.
Al-Mg FSW. Dissimilar welding of Al-Mg was carried out with magnesium alloy
on advancing side and keeping welding parameters same as similar magnesium alloy
FSW with tool offset of 2 mm to magnesium alloy. The weld surface shows smooth
surface finish with little flash on the advancing side (Fig. 4c).
3.2 Bobbin Tool FSW (BTFSW)
Al-Al BTFSW. BTFSW trials were carried initially with similar alloys. Three trials
of BTFSW for similar Al-Al were carried out with 1070 rpm and 20 mm/min feed
speed. Figures 5a, b, d show the top surface of weld with a smooth surface with fine
shoulder marks. With initial two trials, flash was generated on the retreating side after
half of the length welded (Fig. 5a, b). Also, a visible groove mark was observed on
the advancing side of the weld. While the bottom surface was marked with imperfect
shoulder marks of less than shoulder diameter size indicating insufficient contact
with lower shoulder (Fig. 5c, e). There was very less material sticking to tool pin.
These trials suggest the possibility of forming a sound joint with similar Al-Al.