

Processes 2018, 6,82
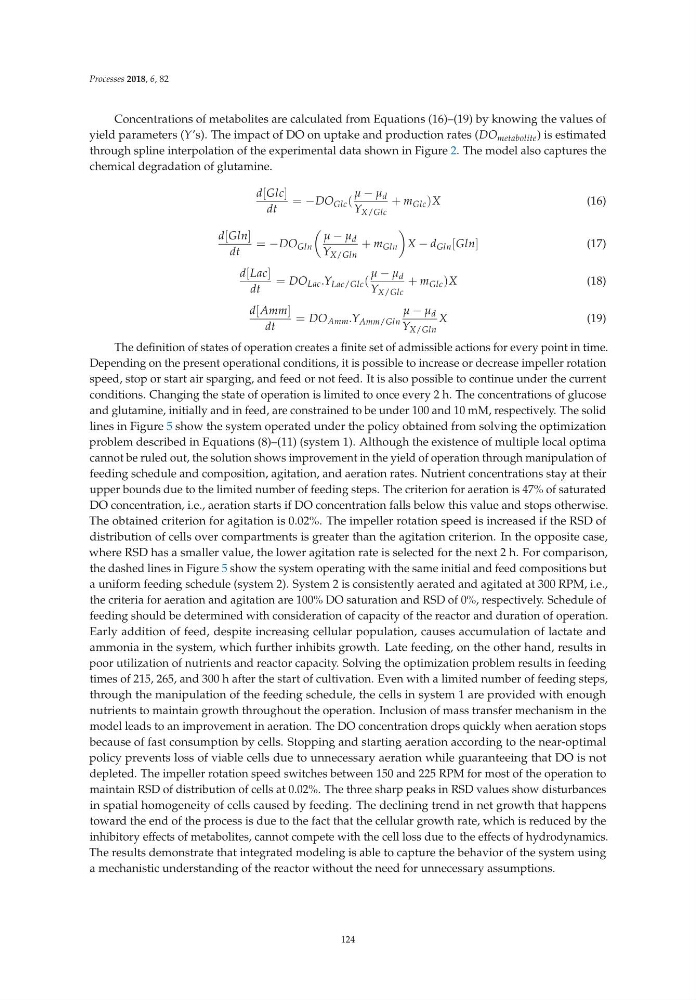
Concentrations of metabolites are calculated from Equations (16)–(19) by knowing the values of
yield parameters (Y’s). The impact of DO on uptake and production rates (DO metabolite ) is estimated
through spline interpolation of the experimental data shown in Figure 2. The model also captures the
chemical degradation of glutamine.
d[Glc]
dt
= −DO Glc (
μ − μ d
Y X/Glc
+ m Glc )X
(16)
d[Gln]
dt
= −DO Gln
μ − μ d
Y X/Gln
+ m Gln
X − d Gln [Gln]
(17)
d[Lac]
dt
= DO Lac .Y Lac/Glc (
μ − μ d
Y X/Glc
+ m Glc )X
(18)
d[Amm]
dt
= DO Amm .Y Amm/Gln
μ − μ d
Y X/Gln
X
(19)
The definition of states of operation creates a finite set of admissible actions for every point in time.
Depending on the present operational conditions, it is possible to increase or decrease impeller rotation
speed, stop or start air sparging, and feed or not feed. It is also possible to continue under the current
conditions. Changing the state of operation is limited to once every 2 h. The concentrations of glucose
and glutamine, initially and in feed, are constrained to be under 100 and 10 mM, respectively. The solid
lines in Figure 5 show the system operated under the policy obtained from solving the optimization
problem described in Equations (8)–(11) (system 1). Although the existence of multiple local optima
cannot be ruled out, the solution shows improvement in the yield of operation through manipulation of
feeding schedule and composition, agitation, and aeration rates. Nutrient concentrations stay at their
upper bounds due to the limited number of feeding steps. The criterion for aeration is 47% of saturated
DO concentration, i.e., aeration starts if DO concentration falls below this value and stops otherwise.
The obtained criterion for agitation is 0.02%. The impeller rotation speed is increased if the RSD of
distribution of cells over compartments is greater than the agitation criterion. In the opposite case,
where RSD has a smaller value, the lower agitation rate is selected for the next 2 h. For comparison,
the dashed lines in Figure 5 show the system operating with the same initial and feed compositions but
a uniform feeding schedule (system 2). System 2 is consistently aerated and agitated at 300 RPM, i.e.,
the criteria for aeration and agitation are 100% DO saturation and RSD of 0%, respectively. Schedule of
feeding should be determined with consideration of capacity of the reactor and duration of operation.
Early addition of feed, despite increasing cellular population, causes accumulation of lactate and
ammonia in the system, which further inhibits growth. Late feeding, on the other hand, results in
poor utilization of nutrients and reactor capacity. Solving the optimization problem results in feeding
times of 215, 265, and 300 h after the start of cultivation. Even with a limited number of feeding steps,
through the manipulation of the feeding schedule, the cells in system 1 are provided with enough
nutrients to maintain growth throughout the operation. Inclusion of mass transfer mechanism in the
model leads to an improvement in aeration. The DO concentration drops quickly when aeration stops
because of fast consumption by cells. Stopping and starting aeration according to the near-optimal
policy prevents loss of viable cells due to unnecessary aeration while guaranteeing that DO is not
depleted. The impeller rotation speed switches between 150 and 225 RPM for most of the operation to
maintain RSD of distribution of cells at 0.02%. The three sharp peaks in RSD values show disturbances
in spatial homogeneity of cells caused by feeding. The declining trend in net growth that happens
toward the end of the process is due to the fact that the cellular growth rate, which is reduced by the
inhibitory effects of metabolites, cannot compete with the cell loss due to the effects of hydrodynamics.
The results demonstrate that integrated modeling is able to capture the behavior of the system using
a mechanistic understanding of the reactor without the need for unnecessary assumptions.
124