

9.2 Transient Coupling Model of Keyhole and Weld Pool in Vacuum
257
In addition, considering the Fresnel multiple reflection absorption, heat radiation,
and evaporation on the free surface under the vacuum condition, the energy boundary
condition can be determined as:
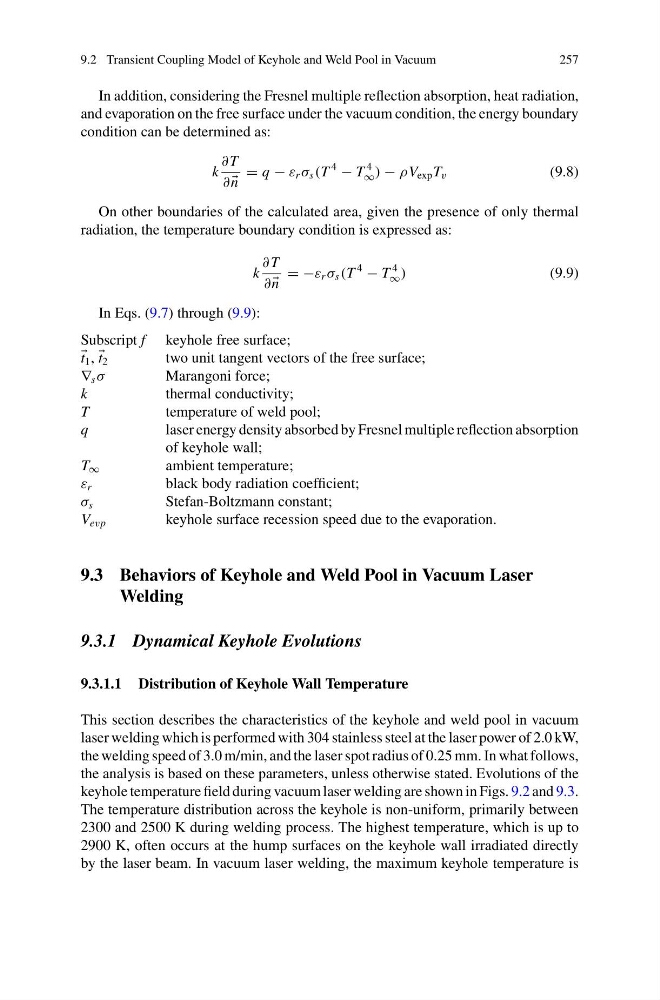
k
∂ T
∂
n
= q − ε r σ s (T
4
− T
4
∞ ) − ρV exp T v
(9.8)
On other boundaries of the calculated area, given the presence of only thermal
radiation, the temperature boundary condition is expressed as:
k
∂ T
∂
n
= −ε r σ s (T
4
− T
4
∞ )
(9.9)
In Eqs. (9.7) through (9.9):
Subscript f keyhole free surface;
t 1 ,
t 2
two unit tangent vectors of the free surface;
∇ s σ
Marangoni force;
k
thermal conductivity;
T
temperature of weld pool;
q
laser energy density absorbed by Fresnel multiple reflection absorption
of keyhole wall;
T ∞
ambient temperature;
ε r
black body radiation coefficient;
σ s
Stefan-Boltzmann constant;
V evp
keyhole surface recession speed due to the evaporation.
9.3 Behaviors of Keyhole and Weld Pool in Vacuum Laser
Welding
9.3.1 Dynamical Keyhole Evolutions
9.3.1.1 Distribution of Keyhole Wall Temperature
This section describes the characteristics of the keyhole and weld pool in vacuum
laser welding which is performed with 304 stainless steel at the laser power of 2.0 kW,
the welding speed of 3.0 m/min, and the laser spot radius of 0.25 mm. In what follows,
the analysis is based on these parameters, unless otherwise stated. Evolutions of the
keyhole temperature field during vacuum laser welding are shown in Figs. 9.2 and 9.3.
The temperature distribution across the keyhole is non-uniform, primarily between
2300 and 2500 K during welding process. The highest temperature, which is up to
2900 K, often occurs at the hump surfaces on the keyhole wall irradiated directly
by the laser beam. In vacuum laser welding, the maximum keyhole temperature is