

8.3 Keyhole and Weld Pool Dynamics in Welding with Filler Wires
219
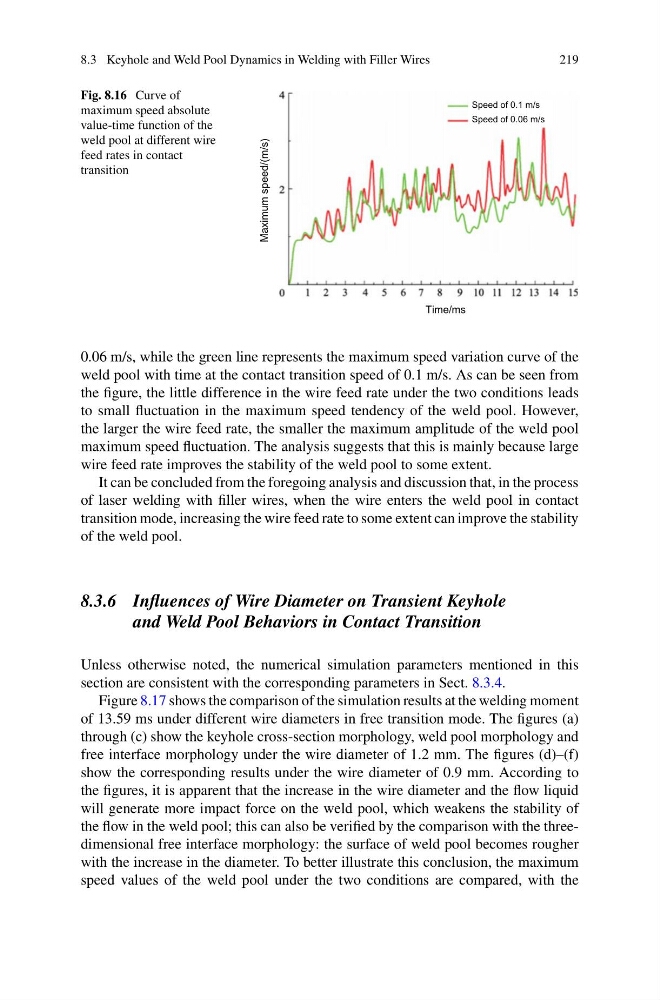
Fig. 8.16 Curve of
maximum speed absolute
value-time function of the
weld pool at different wire
feed rates in contact
transition
Time/ms
Maximum speed/(m/s)
Speed of 0.1 m/s
Speed of 0.06 m/s
0.06 m/s, while the green line represents the maximum speed variation curve of the
weld pool with time at the contact transition speed of 0.1 m/s. As can be seen from
the figure, the little difference in the wire feed rate under the two conditions leads
to small fluctuation in the maximum speed tendency of the weld pool. However,
the larger the wire feed rate, the smaller the maximum amplitude of the weld pool
maximum speed fluctuation. The analysis suggests that this is mainly because large
wire feed rate improves the stability of the weld pool to some extent.
It can be concluded from the foregoing analysis and discussion that, in the process
of laser welding with filler wires, when the wire enters the weld pool in contact
transition mode, increasing the wire feed rate to some extent can improve the stability
of the weld pool.
8.3.6 Influences of Wire Diameter on Transient Keyhole
and Weld Pool Behaviors in Contact Transition
Unless otherwise noted, the numerical simulation parameters mentioned in this
section are consistent with the corresponding parameters in Sect. 8.3.4.
Figure 8.17 shows the comparison of the simulation results at the welding moment
of 13.59 ms under different wire diameters in free transition mode. The figures (a)
through (c) show the keyhole cross-section morphology, weld pool morphology and
free interface morphology under the wire diameter of 1.2 mm. The figures (d)–(f)
show the corresponding results under the wire diameter of 0.9 mm. According to
the figures, it is apparent that the increase in the wire diameter and the flow liquid
will generate more impact force on the weld pool, which weakens the stability of
the flow in the weld pool; this can also be verified by the comparison with the threedimensional free interface morphology: the surface of weld pool becomes rougher
with the increase in the diameter. To better illustrate this conclusion, the maximum
speed values of the weld pool under the two conditions are compared, with the