

218
8 Keyhole and Weld Pool Dynamics in Laser Welding with Filler Wires
wire transits to the surface of the parent metal. The front edge temperature of the
keyhole increases as the metal liquid spreads out. The higher the temperature of
the keyhole front wall, the greater the recoil pressure. Therefore, the wire solution
will flow quickly into the keyhole under the action of recoil pressure, resulting in
instability of the keyhole.
The foregoing simulation results indicate that, if the wire enters the weld pool in
contact transition mode in the process of laser welding with filler wires, the molten
droplet liquid may flow into or be pushed into the keyhole by the recoil pressure to
reduce the stability of the keyhole.
8.3.5 Influences of Wire Feed Speed on Transient Keyhole
and Weld Pool Behaviors in Contact Transition
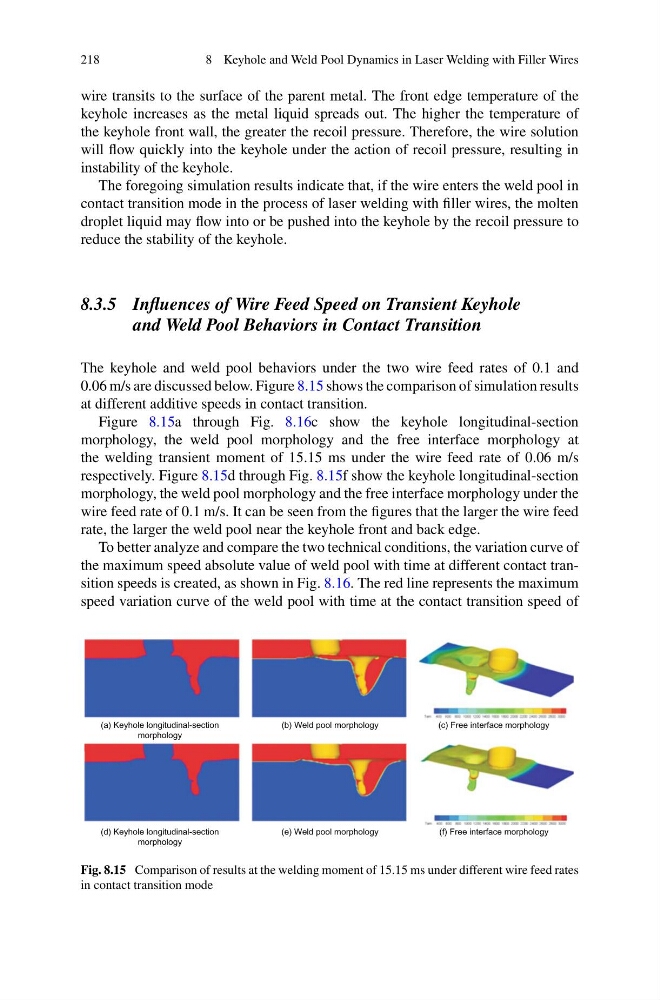
The keyhole and weld pool behaviors under the two wire feed rates of 0.1 and
0.06 m/s are discussed below. Figure 8.15 shows the comparison of simulation results
at different additive speeds in contact transition.
Figure 8.15a through Fig. 8.16c show the keyhole longitudinal-section
morphology, the weld pool morphology and the free interface morphology at
the welding transient moment of 15.15 ms under the wire feed rate of 0.06 m/s
respectively. Figure 8.15d through Fig. 8.15f show the keyhole longitudinal-section
morphology, the weld pool morphology and the free interface morphology under the
wire feed rate of 0.1 m/s. It can be seen from the figures that the larger the wire feed
rate, the larger the weld pool near the keyhole front and back edge.
To better analyze and compare the two technical conditions, the variation curve of
the maximum speed absolute value of weld pool with time at different contact transition speeds is created, as shown in Fig. 8.16. The red line represents the maximum
speed variation curve of the weld pool with time at the contact transition speed of
(d) Keyhole longitudinal-section
morphology
(e) Weld pool morphology
(f) Free interface morphology
(c) Free interface morphology
(b) Weld pool morphology
(a) Keyhole longitudinal-section
morphology
Fig. 8.15 Comparison of results at the welding moment of 15.15 ms under different wire feed rates
in contact transition mode