

7.2 Transient Coupling Model of Keyhole and Weld Pool in Dual-Beam Welding
185
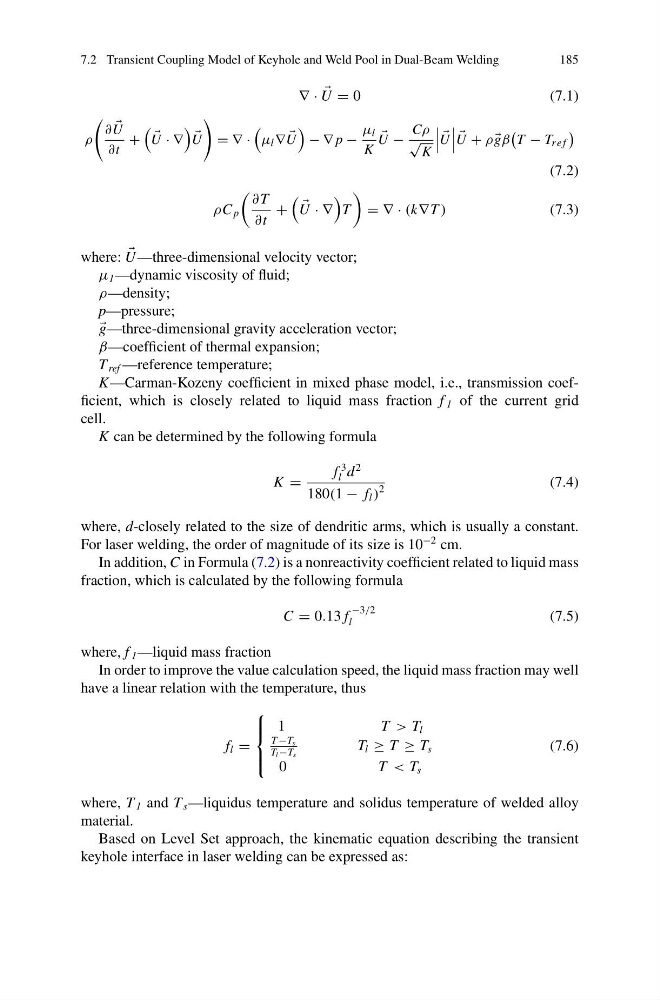
∇ ·
U = 0
(7.1)
ρ
∂
U
∂t
+
U · ∇
U
= ∇ ·
μ l ∇
U
− ∇ p −
μ l
K
U −
Cρ
√
K
U
U + ρ
gβ
T − T re f
(7.2)
ρC p
∂ T
∂t
+
U · ∇
T
= ∇ · (k∇T )
(7.3)
where:
U —three-dimensional velocity vector;
μ 1 —dynamic viscosity of fluid;
ρ—density;
p—pressure;
g—three-dimensional gravity acceleration vector;
β—coefficient of thermal expansion;
T ref —reference temperature;
K—Carman-Kozeny coefficient in mixed phase model, i.e., transmission coefficient, which is closely related to liquid mass fraction f 1 of the current grid
cell.
K can be determined by the following formula
K =
f
3
l d
2
180(1 − f l )
2
(7.4)
where, d-closely related to the size of dendritic arms, which is usually a constant.
For laser welding, the order of magnitude of its size is 10
−2 cm.
In addition, C in Formula (7.2) is a nonreactivity coefficient related to liquid mass
fraction, which is calculated by the following formula
C = 0.13 f
−3/2
l
(7.5)
where, f 1 —liquid mass fraction
In order to improve the value calculation speed, the liquid mass fraction may well
have a linear relation with the temperature, thus
f l =
⎧
⎪ ⎨
⎪ ⎩
1
T > T l
T −T s
T l −T s
T l ≥ T ≥ T s
0
T < T s
(7.6)
where, T 1 and T s —liquidus temperature and solidus temperature of welded alloy
material.
Based on Level Set approach, the kinematic equation describing the transient
keyhole interface in laser welding can be expressed as: