

4.3 Effects of Physical Factors on the Coupling Behavior
135
Time/ms
Time/ms
Keyhole depth/mm)
Keyhole depth/mm)
(a) Time from 0 ms to 30 ms
(b) Time from 20 ms to 25 ms
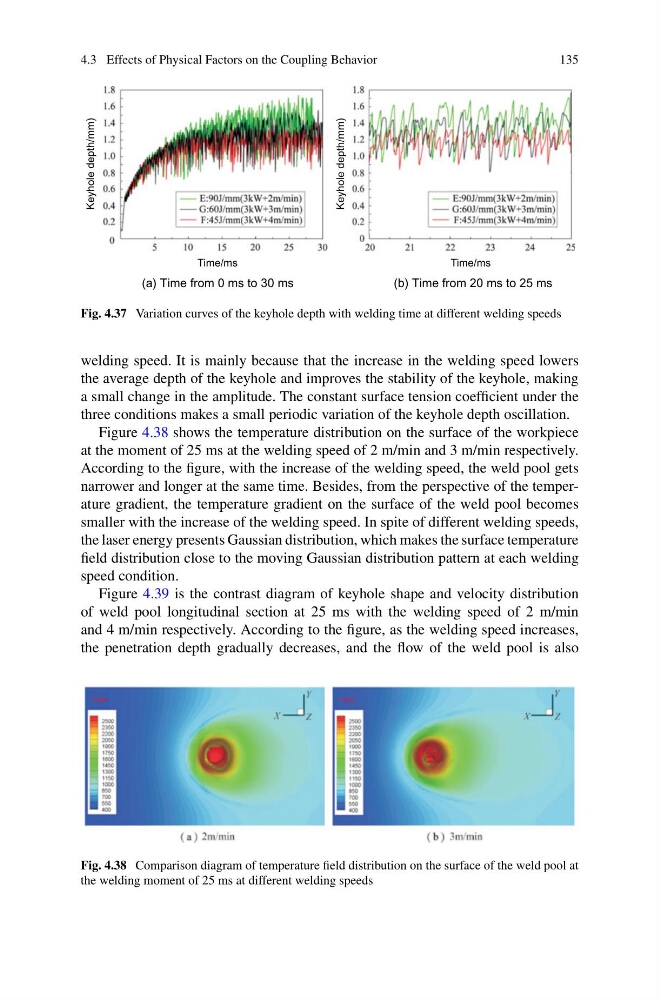
Fig. 4.37 Variation curves of the keyhole depth with welding time at different welding speeds
welding speed. It is mainly because that the increase in the welding speed lowers
the average depth of the keyhole and improves the stability of the keyhole, making
a small change in the amplitude. The constant surface tension coefficient under the
three conditions makes a small periodic variation of the keyhole depth oscillation.
Figure 4.38 shows the temperature distribution on the surface of the workpiece
at the moment of 25 ms at the welding speed of 2 m/min and 3 m/min respectively.
According to the figure, with the increase of the welding speed, the weld pool gets
narrower and longer at the same time. Besides, from the perspective of the temperature gradient, the temperature gradient on the surface of the weld pool becomes
smaller with the increase of the welding speed. In spite of different welding speeds,
the laser energy presents Gaussian distribution, which makes the surface temperature
field distribution close to the moving Gaussian distribution pattern at each welding
speed condition.
Figure 4.39 is the contrast diagram of keyhole shape and velocity distribution
of weld pool longitudinal section at 25 ms with the welding speed of 2 m/min
and 4 m/min respectively. According to the figure, as the welding speed increases,
the penetration depth gradually decreases, and the flow of the weld pool is also
Fig. 4.38 Comparison diagram of temperature field distribution on the surface of the weld pool at
the welding moment of 25 ms at different welding speeds