

308
T. M. N. T. Anuwa et al.
until the metal joins in solid-state. The combination of heat generated by friction and
consequent plastic deformation being the main causes of fusion.
Besides, the development of FSW by TWI in the UK is better compared to gas
metal arc welding (GMAW) and gas tungsten arc welding (GTAW). It is because the
FSW method is free from various types of defects. The conventional milling machine
MILKO 37 is chosen to innovate and become a FSW machine to run the process.
One of the limitations is the existence exit hole at the end of the joining process
by FSW. Nowadays, FSW is also found in modern shipyard, trains, automotive, and
aerospace applications [2].
The FSW process is suitable for various joining configurations such as butt joint
and lap joint [3]. This welding process requires no edge preparation. No shielding gas
is required for the materials such as aluminum at which this process only generates
friction from the non-consumable welding tool. A backing plate was mostly needed
before the material is welded to the parts so that the faces are rigidly fixed to each
other to be welded [4].
29.2 Experimental Setup
The work is performed using distinct parameters to achieve the optimum configuration of the parameters in terms of performance, macrostructure, and tensile strength.
Each parameter used during the operation will produce good outputs. The chemical
composition and mechanical properties of the AA5052-H32 delivered by Atlas Steels
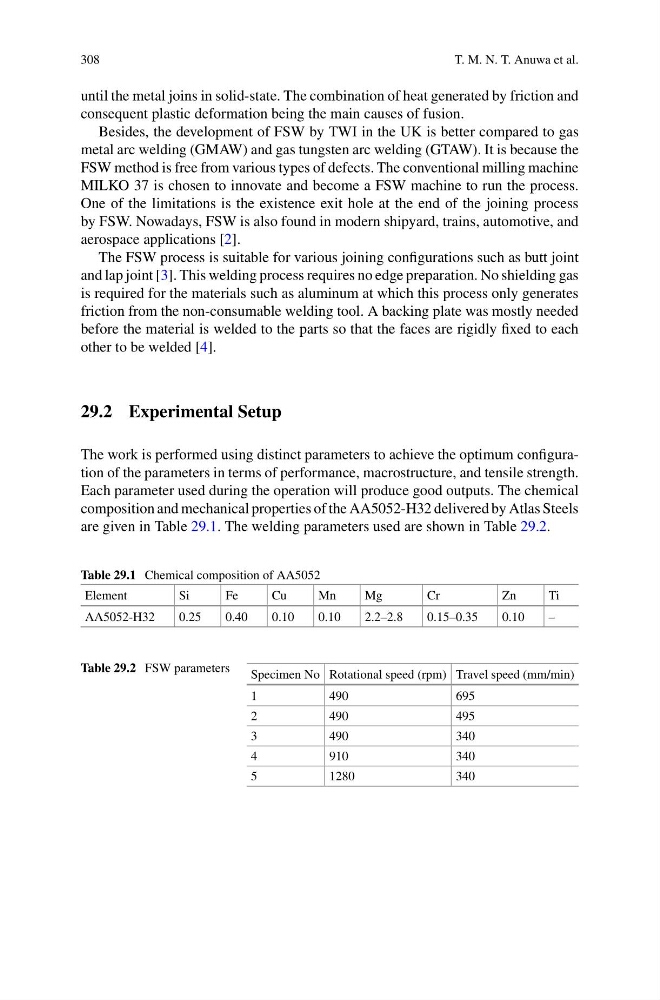
are given in Table 29.1. The welding parameters used are shown in Table 29.2.
Table 29.1 Chemical composition of AA5052
Element
Si
Fe
Cu
Mn
Mg
Cr
Zn
Ti
AA5052-H32
0.25
0.40
0.10
0.10
2.2–2.8
0.15–0.35
0.10
–
Table 29.2 FSW parameters
Specimen No Rotational speed (rpm) Travel speed (mm/min)
1
490
695
2
490
495
3
490
340
4
910
340
5
1280
340