

28 Optimization of Welding Parameters for Self-Support …
303
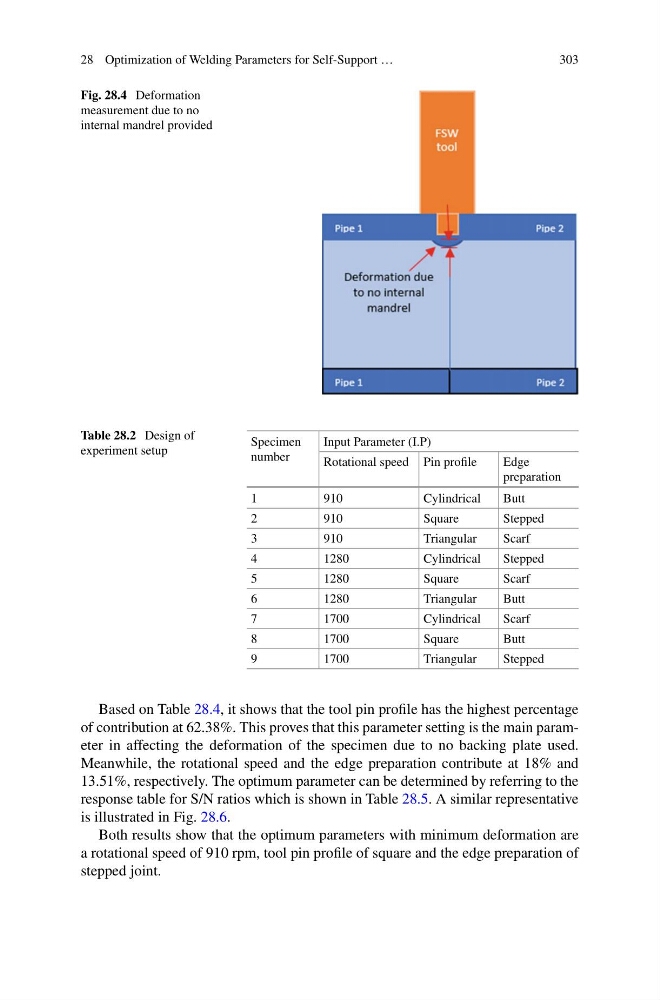
Fig. 28.4 Deformation
measurement due to no
internal mandrel provided
Table 28.2 Design of
experiment setup
Specimen
number
Input Parameter (I.P)
Rotational speed Pin profile
Edge
preparation
1
910
Cylindrical
Butt
2
910
Square
Stepped
3
910
Triangular
Scarf
4
1280
Cylindrical
Stepped
5
1280
Square
Scarf
6
1280
Triangular
Butt
7
1700
Cylindrical
Scarf
8
1700
Square
Butt
9
1700
Triangular
Stepped
Based on Table 28.4, it shows that the tool pin profile has the highest percentage
of contribution at 62.38%. This proves that this parameter setting is the main parameter in affecting the deformation of the specimen due to no backing plate used.
Meanwhile, the rotational speed and the edge preparation contribute at 18% and
13.51%, respectively. The optimum parameter can be determined by referring to the
response table for S/N ratios which is shown in Table 28.5. A similar representative
is illustrated in Fig. 28.6.
Both results show that the optimum parameters with minimum deformation are
a rotational speed of 910 rpm, tool pin profile of square and the edge preparation of
stepped joint.