

296
M. A. A. A. Razak et al.
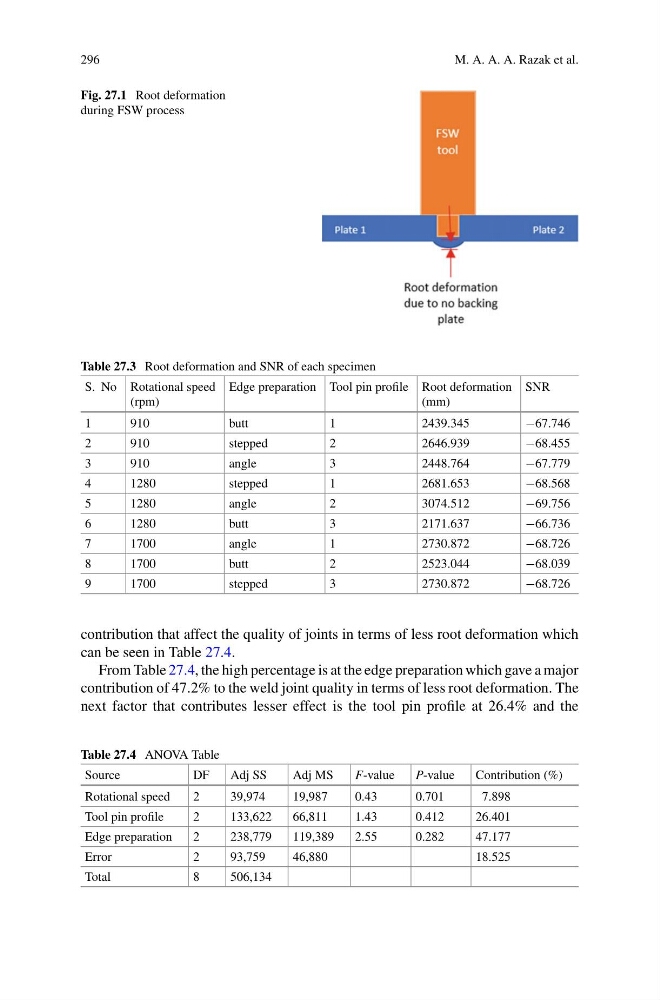
Fig. 27.1 Root deformation
during FSW process
Table 27.3 Root deformation and SNR of each specimen
S. No Rotational speed
(rpm)
Edge preparation Tool pin profile Root deformation
(mm)
SNR
1
910
butt
1
2439.345
−67.746
2
910
stepped
2
2646.939
−68.455
3
910
angle
3
2448.764
−67.779
4
1280
stepped
1
2681.653
−68.568
5
1280
angle
2
3074.512
−69.756
6
1280
butt
3
2171.637
−66.736
7
1700
angle
1
2730.872
−68.726
8
1700
butt
2
2523.044
−68.039
9
1700
stepped
3
2730.872
−68.726
contribution that affect the quality of joints in terms of less root deformation which
can be seen in Table 27.4.
From Table 27.4, the high percentage is at the edge preparation which gave a major
contribution of 47.2% to the weld joint quality in terms of less root deformation. The
next factor that contributes lesser effect is the tool pin profile at 26.4% and the
Table 27.4 ANOVA Table
Source
DF
Adj SS
Adj MS
F-value
P-value
Contribution (%)
Rotational speed
2
39,974
19,987
0.43
0.701
7.898
Tool pin profile
2
133,622
66,811
1.43
0.412
26.401
Edge preparation
2
238,779
119,389
2.55
0.282
47.177
Error
2
93,759
46,880
18.525
Total
8
506,134