

27 Experimental Study on Self-Supported …
295
Table 27.1 Welding
parameters
S. No Rotational speed
(rpm)
Edge preparation Tool pin profile
1
910
butt
1
2
910
stepped
2
3
910
angle
3
4
1280
stepped
1
5
1280
angle
2
6
1280
butt
3
7
1700
angle
1
8
1700
butt
2
9
1700
stepped
3
Table 27.2 Tool pin profiles
Number tool Description of
the tool
Length of the
pin (mm)
Inner diameter
of the pin (mm)
Outer
diameter of
the pin (mm)
Diameter of
the shoulder
(mm)
1
Cylindrical
tapered
4
3
5
20
2
Square tapered 4
3
5
20
3
Triangular
tapered
4
3
5
20
of experiments. By using Taguchi method, the number of the experiment tested will
decrease significantly [11–13].
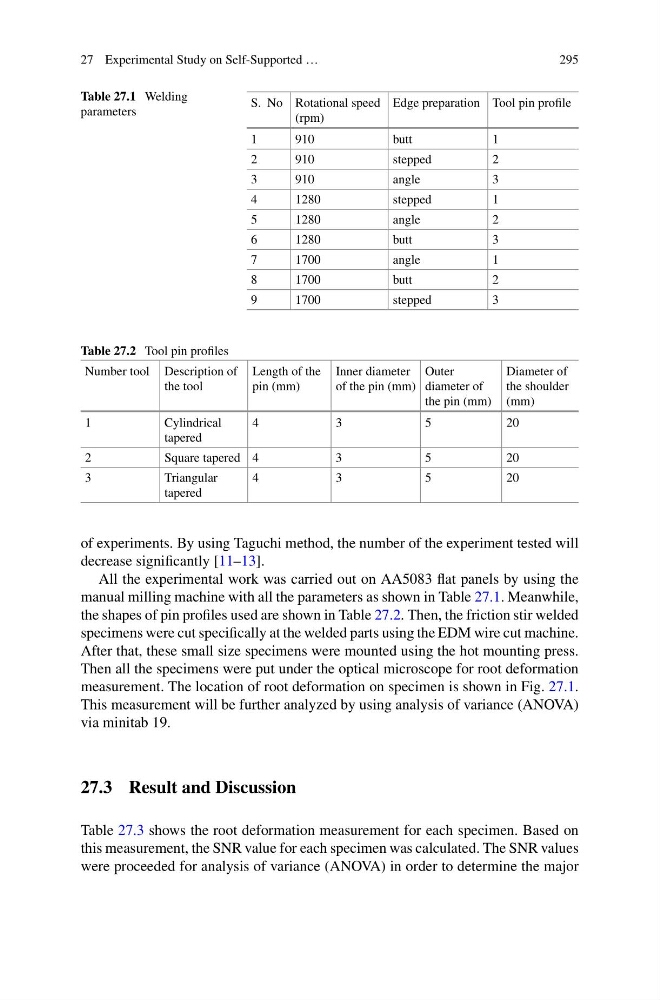
All the experimental work was carried out on AA5083 flat panels by using the
manual milling machine with all the parameters as shown in Table 27.1. Meanwhile,
the shapes of pin profiles used are shown in Table 27.2. Then, the friction stir welded
specimens were cut specifically at the welded parts using the EDM wire cut machine.
After that, these small size specimens were mounted using the hot mounting press.
Then all the specimens were put under the optical microscope for root deformation
measurement. The location of root deformation on specimen is shown in Fig. 27.1.
This measurement will be further analyzed by using analysis of variance (ANOVA)
via minitab 19.
27.3 Result and Discussion
Table 27.3 shows the root deformation measurement for each specimen. Based on
this measurement, the SNR value for each specimen was calculated. The SNR values
were proceeded for analysis of variance (ANOVA) in order to determine the major