

542
A. Jadhav and S. Kumar
speed was important and significant factor before laser power assists gas to minimize dross height. Interactions between them are also significant. A quadratic value
of cutting speed is other significant parameter.
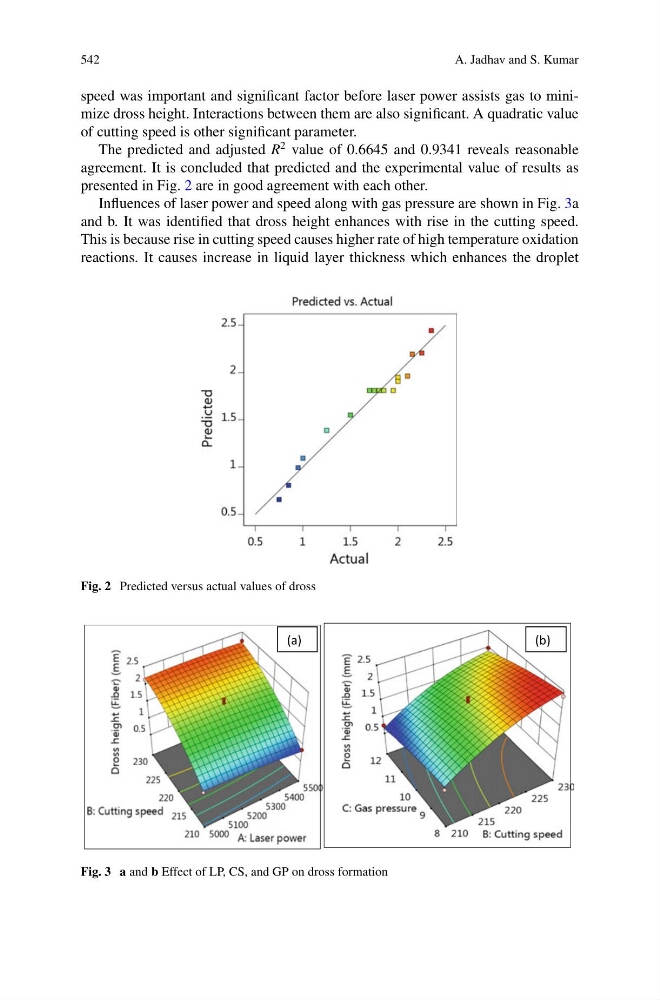
The predicted and adjusted R
2 value of 0.6645 and 0.9341 reveals reasonable
agreement. It is concluded that predicted and the experimental value of results as
presented in Fig. 2 are in good agreement with each other.
Influences of laser power and speed along with gas pressure are shown in Fig. 3a
and b. It was identified that dross height enhances with rise in the cutting speed.
This is because rise in cutting speed causes higher rate of high temperature oxidation
reactions. It causes increase in liquid layer thickness which enhances the droplet
Fig. 2 Predicted versus actual values of dross
(a)
(b)
Fig. 3 a and b Effect of LP, CS, and GP on dross formation