

6.3 Application in the Defence Industry
91
Table 6.3 Production
volume and sequence of
machines for each part
Production
Part volume
Machine sequence
P01 100
M1-M4-M2-M6
P02 120
M3-M5-M12-M10
P03
50
M2-M4-M12-M6
P04
45
M5-M8-M10
P05
60
M3-M5-M12-M6
P06
80
M4-M2-M4-M6
P07
90
M1-M5-M9
P08 120
M3-M7-M10-M4-M8
P09 140
M1-M4-M6
P10 180
M3-M12-M8-M10
P11
80
M2-M6-M2-M4-M6
P12
60
M11-M9-M10-M8
P13
70
M1-M4-M5-M7
P14 150
M2-M4-M6-M2-M6
P15 120
M3-M7-M9-M10
P16 120
M3-M10-M12-M9-M12
P17 100
M5-M10-M8-M9-M12
P18
90
M2-M8-M9-M10
6.3 Application in the Defence Industry
This section presents one application among many in the area of defence: the
production of wheel arm brackets for defence vehicles. There are two components
per bracket and a total of eight machines; each machine carries out a specific
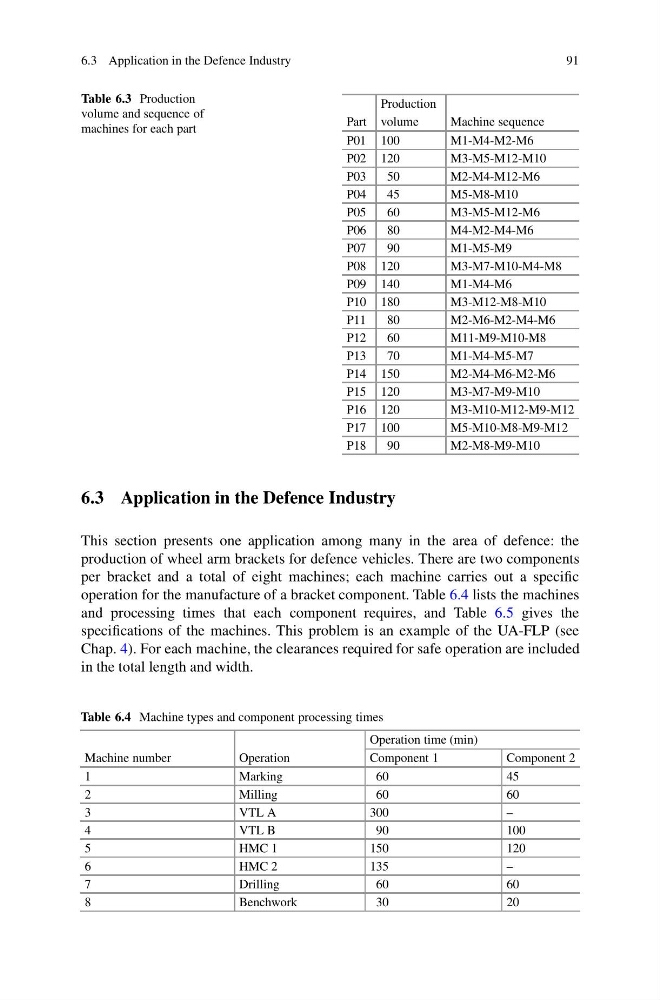
operation for the manufacture of a bracket component. Table 6.4 lists the machines
and processing times that each component requires, and Table 6.5 gives the
specifications of the machines. This problem is an example of the UA-FLP (see
Chap. 4). For each machine, the clearances required for safe operation are included
in the total length and width.
Table 6.4 Machine types and component processing times
Operation time (min)
Machine number
Operation
Component 1
Component 2
1
Marking
60
45
2
Milling
60
60
3
VTL A
300
–
4
VTL B
90
100
5
HMC 1
150
120
6
HMC 2
135
–
7
Drilling
60
60
8
Benchwork
30
20