

522
The Chemistry and Technology of Petroleum
As an integrated conversion block, residue hydrotreating and RFCC complement each other and
can offset many of the inherent deficiencies related to residue conversion.
19.4.1 AsPHAlt resIduAl treAtIng ProCess
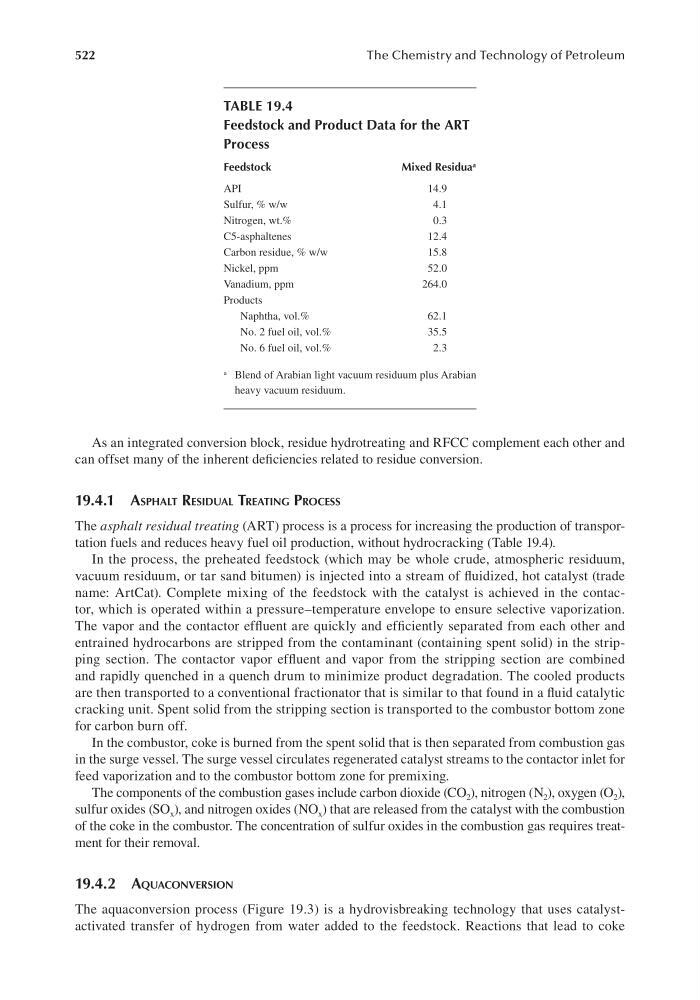
The asphalt residual treating (ART) process is a process for increasing the production of transportation fuels and reduces heavy fuel oil production, without hydrocracking (Table 19.4).
In the process, the preheated feedstock (which may be whole crude, atmospheric residuum,
vacuum residuum, or tar sand bitumen) is injected into a stream of fluidized, hot catalyst (trade
name: ArtCat). Complete mixing of the feedstock with the catalyst is achieved in the contactor, which is operated within a pressure–temperature envelope to ensure selective vaporization.
The vapor and the contactor effluent are quickly and efficiently separated from each other and
entrained hydrocarbons are stripped from the contaminant (containing spent solid) in the stripping section. The contactor vapor effluent and vapor from the stripping section are combined
and rapidly quenched in a quench drum to minimize product degradation. The cooled products
are then transported to a conventional fractionator that is similar to that found in a fluid catalytic
cracking unit. Spent solid from the stripping section is transported to the combustor bottom zone
for carbon burn off.
In the combustor, coke is burned from the spent solid that is then separated from combustion gas
in the surge vessel. The surge vessel circulates regenerated catalyst streams to the contactor inlet for
feed vaporization and to the combustor bottom zone for premixing.
The components of the combustion gases include carbon dioxide (CO 2 ), nitrogen (N 2 ), oxygen (O 2 ),
sulfur oxides (SO x ), and nitrogen oxides (NO x ) that are released from the catalyst with the combustion
of the coke in the combustor. The concentration of sulfur oxides in the combustion gas requires treatment for their removal.
19.4.2 AQuAConversIon
The aquaconversion process (Figure 19.3) is a hydrovisbreaking technology that uses catalystactivated transfer of hydrogen from water added to the feedstock. Reactions that lead to coke
TABLE 19.4
Feedstock and Product Data for the ART
Process
Feedstock
Mixed Residua a
API
14.9
Sulfur, % w/w
4.1
Nitrogen, wt.%
0.3
C5-asphaltenes
12.4
Carbon residue, % w/w
15.8
Nickel, ppm
52.0
Vanadium, ppm
264.0
Products
Naphtha, vol.%
62.1
No. 2 fuel oil, vol.%
35.5
No. 6 fuel oil, vol.%
2.3
a Blend of Arabian light vacuum residuum plus Arabian
heavy vacuum residuum.