

• Shift condensate rate
This falls out of the material balances as 2, 378 mols/h (leftover process
steam) = 42.3 Mlb/h or $85 gpm.
• Actual steam/carbon ratio
This also fell out of the calculations as X = 4.53.
• Normalized pressure drop
For normalizing the pressure drop, prior history and a normalization basis
(reference conditions) are required. Here, from prior development work, the
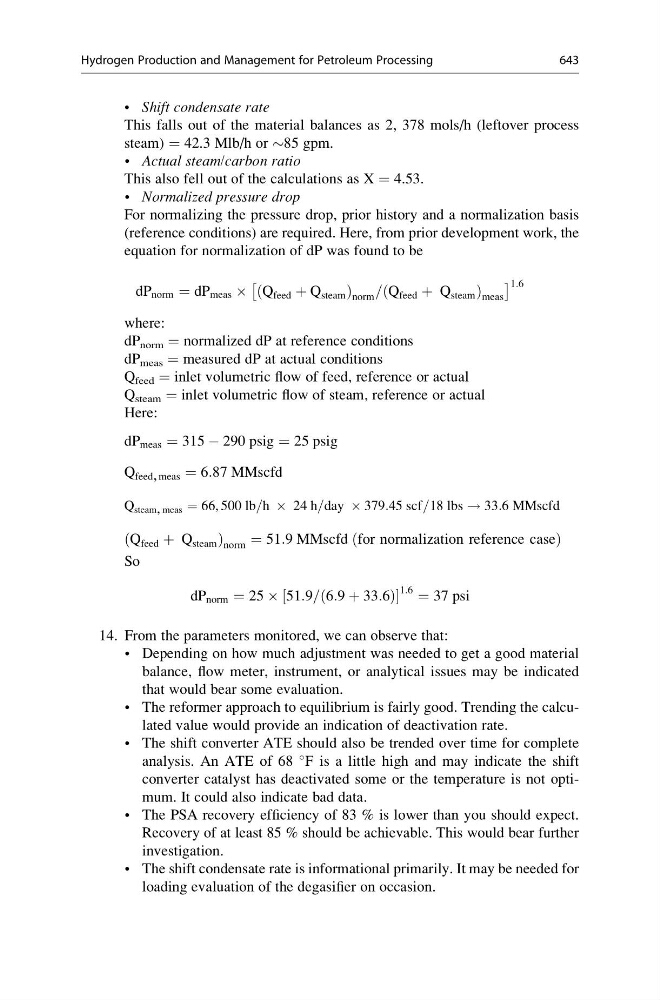
equation for normalization of dP was found to be
dP norm ¼ dP meas  Q feed þ Q steam
ð
Þ norm = Q feed þ Q steam
ð
Þ meas
Â
à 1:6
where:
dP norm = normalized dP at reference conditions
dP meas = measured dP at actual conditions
Q feed = inlet volumetric flow of feed, reference or actual
Q steam = inlet volumetric flow of steam, reference or actual
Here:
dP meas ¼ 315 À 290 psig ¼ 25 psig
Q feed, meas ¼ 6:87 MMscfd
Q steam, meas ¼ 66, 500 lb=h  24 h=day  379:45 scf=18 lbs ! 33:6 MMscfd
Q feed þ Q steam
ð
Þ norm ¼ 51:9 MMscfd ðfor normalization reference caseÞ
So
dP norm ¼ 25 Â 51:9= 6:9 þ 33:6
ð
Þ
½
1:6 ¼ 37 psi
14. From the parameters monitored, we can observe that:
• Depending on how much adjustment was needed to get a good material
balance, flow meter, instrument, or analytical issues may be indicated
that would bear some evaluation.
• The reformer approach to equilibrium is fairly good. Trending the calculated value would provide an indication of deactivation rate.
• The shift converter ATE should also be trended over time for complete
analysis. An ATE of 68
F is a little high and may indicate the shift
converter catalyst has deactivated some or the temperature is not optimum. It could also indicate bad data.
• The PSA recovery efficiency of 83 % is lower than you should expect.
Recovery of at least 85 % should be achievable. This would bear further
investigation.
• The shift condensate rate is informational primarily. It may be needed for
loading evaluation of the degasifier on occasion.
Hydrogen Production and Management for Petroleum Processing
643