

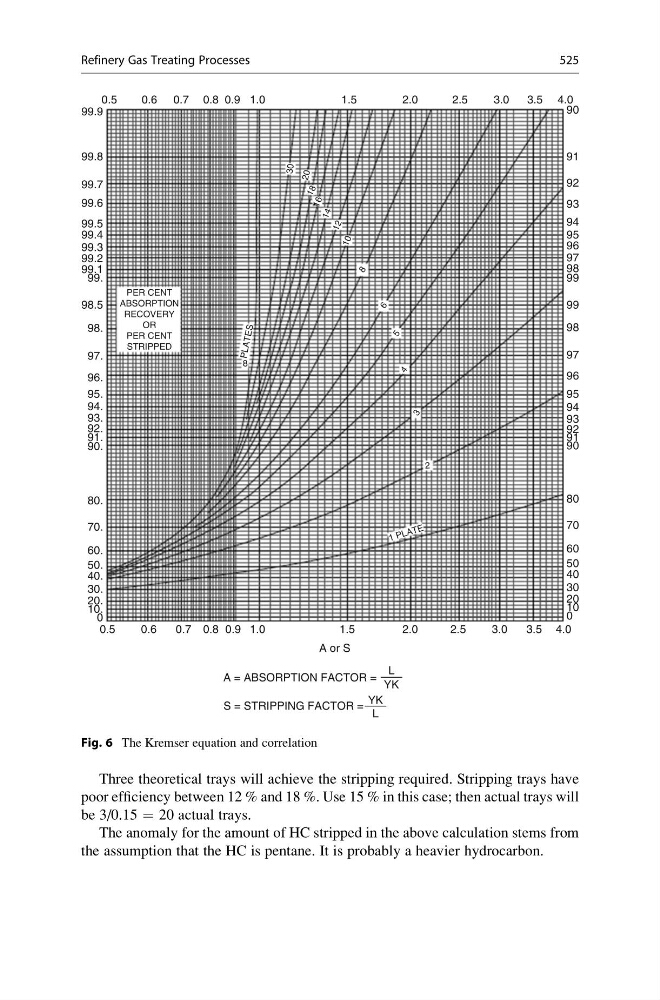
Three theoretical trays will achieve the stripping required. Stripping trays have
poor efficiency between 12 % and 18 %. Use 15 % in this case; then actual trays will
be 3/0.15 = 20 actual trays.
The anomaly for the amount of HC stripped in the above calculation stems from
the assumption that the HC is pentane. It is probably a heavier hydrocarbon.
L
YK
0.5
99.9
0.6 0.7 0.8 0.9 1.0
1.5
2.0
2.5
3.0
3.5 4.0
0.5
0.6
0.7 0.8 0.9
A = ABSORPTION FACTOR =
A or S
S = STRIPPING FACTOR =
1.0
1.5
2.0
2.5
3.0
3.5 4.0
99.8
99.7
99.6
99.5
99.4
99.3
99.2
99.1
98.5
98.
97.
96.
95.
94.
93.
92.
91.
90.
80.
70.
60.
50.
40.
30.
20.
10.
0
99.
PER CENT
ABSORPTION
RECOVERY
OR
PER CENT
STRIPPED
30
20 1 8 1 6
1 4 1 2
1 0 8
6
8
PL AT ES
5
4
3
2
1 P LA T E
90
91
92
93
94
95
96
97
98
99
98
97
96
95
94
93
92
91
90
80
70
60
50
40
30
20
10
0
99
L
YK
Fig. 6 The Kremser equation and correlation
Refinery Gas Treating Processes
525