

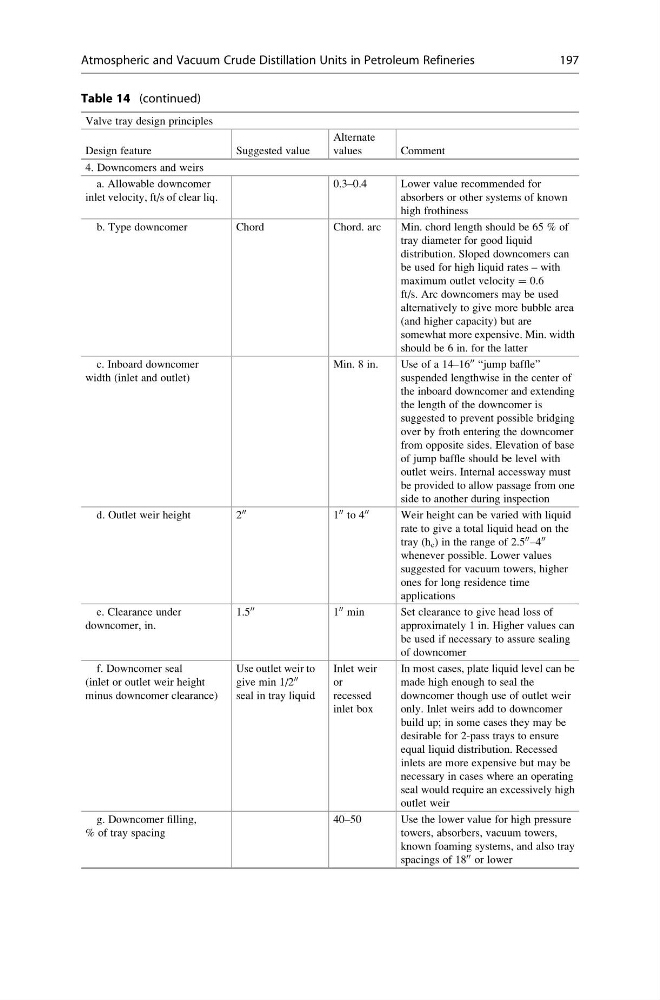
Table 14 (continued)
Valve tray design principles
Design feature
Suggested value
Alternate
values
Comment
4. Downcomers and weirs
a. Allowable downcomer
inlet velocity, ft/s of clear liq.
0.3–0.4
Lower value recommended for
absorbers or other systems of known
high frothiness
b. Type downcomer
Chord
Chord. arc
Min. chord length should be 65 % of
tray diameter for good liquid
distribution. Sloped downcomers can
be used for high liquid rates – with
maximum outlet velocity = 0.6
ft/s. Arc downcomers may be used
alternatively to give more bubble area
(and higher capacity) but are
somewhat more expensive. Min. width
should be 6 in. for the latter
c. Inboard downcomer
width (inlet and outlet)
Min. 8 in.
Use of a 14–16
00 “jump baffle”
suspended lengthwise in the center of
the inboard downcomer and extending
the length of the downcomer is
suggested to prevent possible bridging
over by froth entering the downcomer
from opposite sides. Elevation of base
of jump baffle should be level with
outlet weirs. Internal accessway must
be provided to allow passage from one
side to another during inspection
d. Outlet weir height
2
00
1
00 to 4
00
Weir height can be varied with liquid
rate to give a total liquid head on the
tray (h c ) in the range of 2.5
00 –4
00
whenever possible. Lower values
suggested for vacuum towers, higher
ones for long residence time
applications
e. Clearance under
downcomer, in.
1.5
00
1
00 min
Set clearance to give head loss of
approximately 1 in. Higher values can
be used if necessary to assure sealing
of downcomer
f. Downcomer seal
(inlet or outlet weir height
minus downcomer clearance)
Use outlet weir to
give min 1/2
00
seal in tray liquid
Inlet weir
or
recessed
inlet box
In most cases, plate liquid level can be
made high enough to seal the
downcomer though use of outlet weir
only. Inlet weirs add to downcomer
build up; in some cases they may be
desirable for 2-pass trays to ensure
equal liquid distribution. Recessed
inlets are more expensive but may be
necessary in cases where an operating
seal would require an excessively high
outlet weir
g. Downcomer filling,
% of tray spacing
40–50
Use the lower value for high pressure
towers, absorbers, vacuum towers,
known foaming systems, and also tray
spacings of 18
00 or lower
Atmospheric and Vacuum Crude Distillation Units in Petroleum Refineries
197