

Liquid product drawoff plus stripout leaving to stripper (if applicable)
Liquid overflow from the PA drawoff tray
The pumparound duty in Btu/h
In these items the only unknown is the enthalpy and therefore the temperature of
the vapor leaving the top pumparound tray. Equate heat in = heat out to solve the
unknown.
Step 5. With the duty of the pumparound section in Btu/h and the temperatures in
and out now known, the pumparound section can be treated as a heat exchanger.
The area of heat transfer will be the total tray areas of the section, and the heat
transfer coefficient in terms of Btu/h/sqft/
F is given in Fig. 12.
Step 6. The area is now calculated from the heat transfer equation:
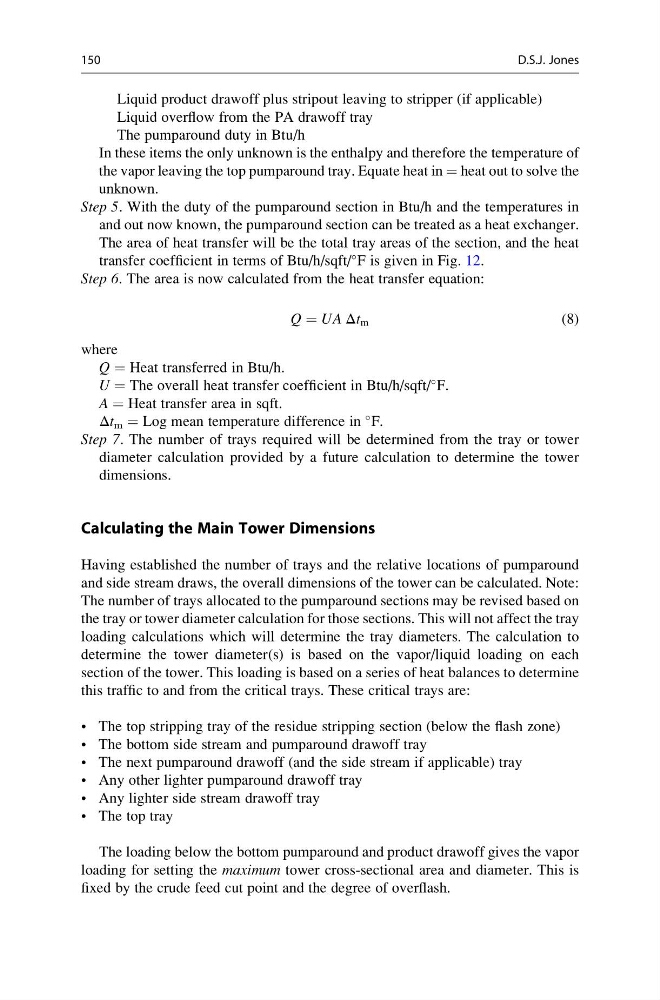
Q ¼ UA Δt m
(8)
where
Q = Heat transferred in Btu/h.
U = The overall heat transfer coefficient in Btu/h/sqft/
F.
A = Heat transfer area in sqft.
Δt m = Log mean temperature difference in
F.
Step 7. The number of trays required will be determined from the tray or tower
diameter calculation provided by a future calculation to determine the tower
dimensions.
Calculating the Main Tower Dimensions
Having established the number of trays and the relative locations of pumparound
and side stream draws, the overall dimensions of the tower can be calculated. Note:
The number of trays allocated to the pumparound sections may be revised based on
the tray or tower diameter calculation for those sections. This will not affect the tray
loading calculations which will determine the tray diameters. The calculation to
determine the tower diameter(s) is based on the vapor/liquid loading on each
section of the tower. This loading is based on a series of heat balances to determine
this traffic to and from the critical trays. These critical trays are:
• The top stripping tray of the residue stripping section (below the flash zone)
• The bottom side stream and pumparound drawoff tray
• The next pumparound drawoff (and the side stream if applicable) tray
• Any other lighter pumparound drawoff tray
• Any lighter side stream drawoff tray
• The top tray
The loading below the bottom pumparound and product drawoff gives the vapor
loading for setting the maximum tower cross-sectional area and diameter. This is
fixed by the crude feed cut point and the degree of overflash.
150
D.S.J. Jones