

164
6 Experimental Validation of the Methodology
The two considered production lines consist of five machines each, with three
machines actually performing machining processes on the product and two machines per line being installed for loading and unloading processes. The machines
per line are strongly linked to each other without any buffers between the single
machines. A machine stoppage for one production machine causes a production
stop for the entire line. In terms of machine logic, all machines have a similar
complexity that corresponds to the high complex machine logic type. All machines have a main switch that can either be on or off, a Programmable Logic
Controller (PLC) that can either be turned on or off, and an operating mode
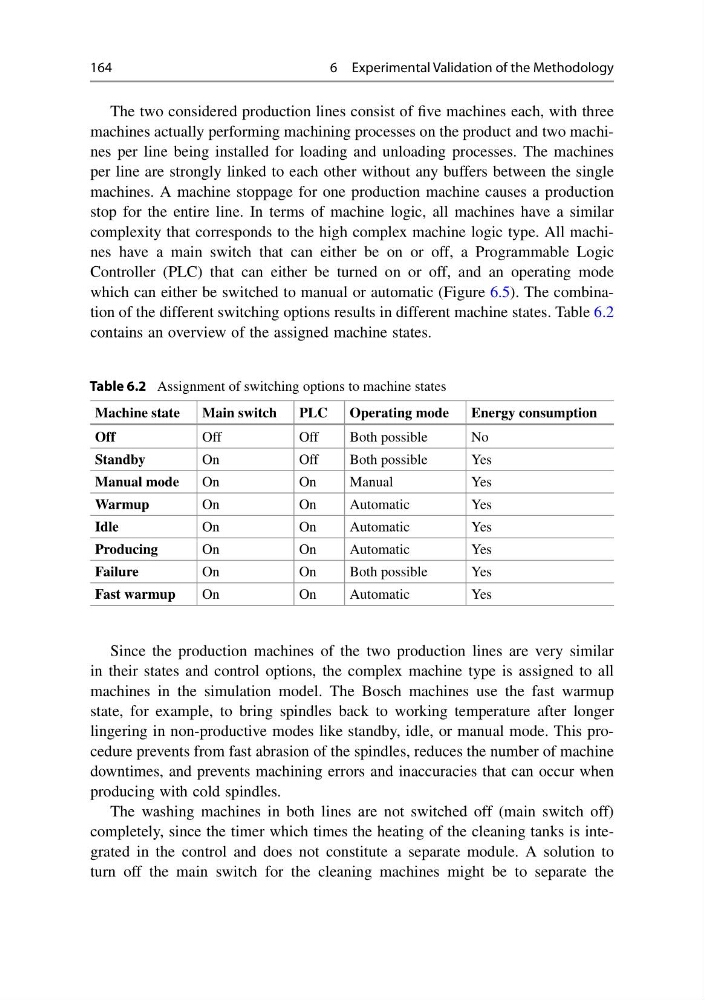
which can either be switched to manual or automatic (Figure 6.5). The combination of the different switching options results in different machine states. Table 6.2
contains an overview of the assigned machine states.
Table 6.2 Assignment of switching options to machine states
Machine state
Main switch
PLC
Operating mode
Energy consumption
Off
Off
Off
Both possible
No
Standby
On
Off
Both possible
Yes
Manual mode
On
On
Manual
Yes
Warmup
On
On
Automatic
Yes
Idle
On
On
Automatic
Yes
Producing
On
On
Automatic
Yes
Failure
On
On
Both possible
Yes
Fast warmup
On
On
Automatic
Yes
Since the production machines of the two production lines are very similar
in their states and control options, the complex machine type is assigned to all
machines in the simulation model. The Bosch machines use the fast warmup
state, for example, to bring spindles back to working temperature after longer
lingering in non-productive modes like standby, idle, or manual mode. This procedure prevents from fast abrasion of the spindles, reduces the number of machine
downtimes, and prevents machining errors and inaccuracies that can occur when
producing with cold spindles.
The washing machines in both lines are not switched off (main switch off)
completely, since the timer which times the heating of the cleaning tanks is integrated in the control and does not constitute a separate module. A solution to
turn off the main switch for the cleaning machines might be to separate the