

3.3 Example
Geometry and
Mechanical
Characterization
In the following example, details will be provided for the
manufacturing of a rectangular specimen with functional graded
features along its major side and for its mechanical characterization.
The protocol shall be adapted for the manufacturing of complexshaped objects.
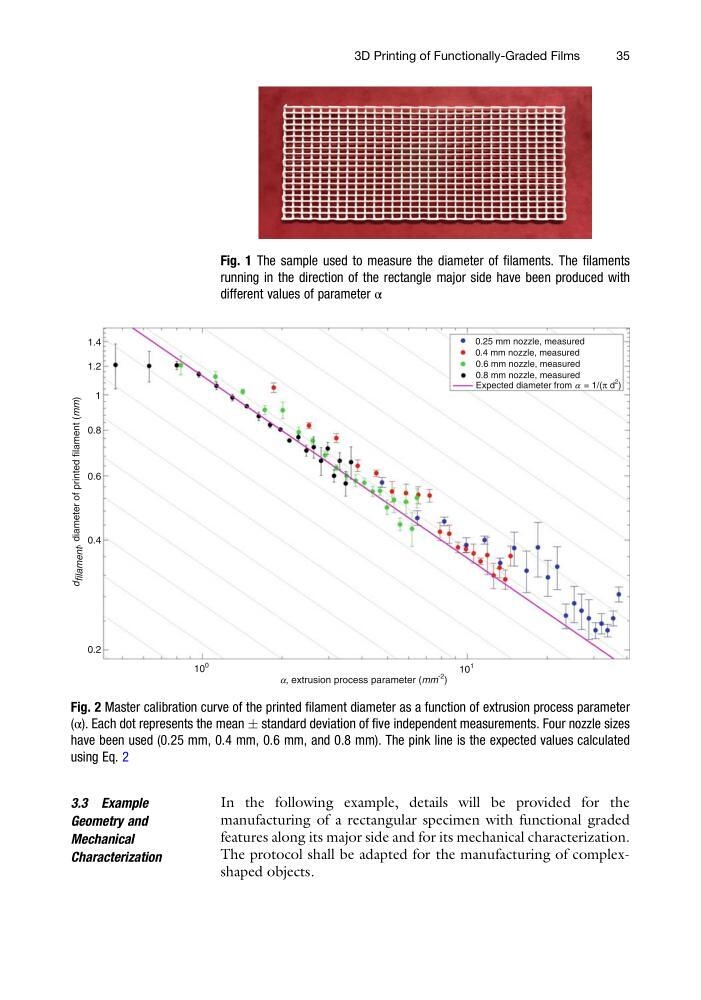
Fig. 1 The sample used to measure the diameter of filaments. The filaments
running in the direction of the rectangle major side have been produced with
different values of parameter α
1.4
1.2
1
0.8
0.6
0.4
0.2
0.25 mm nozzle, measured
0.4 mm nozzle, measured
0.6 mm nozzle, measured
0.8 mm nozzle, measured
Expected diameter from a = 1/(π d
2 )
10
0
10
1
a, extrusion process parameter (mm
-2
)
d
filament , diameter of printed filament (mm)
Fig. 2 Master calibration curve of the printed filament diameter as a function of extrusion process parameter
(α). Each dot represents the mean Æ standard deviation of five independent measurements. Four nozzle sizes
have been used (0.25 mm, 0.4 mm, 0.6 mm, and 0.8 mm). The pink line is the expected values calculated
using Eq. 2
3D Printing of Functionally-Graded Films
35