

17 Microplane Modeling for Inelastic Responses …
321
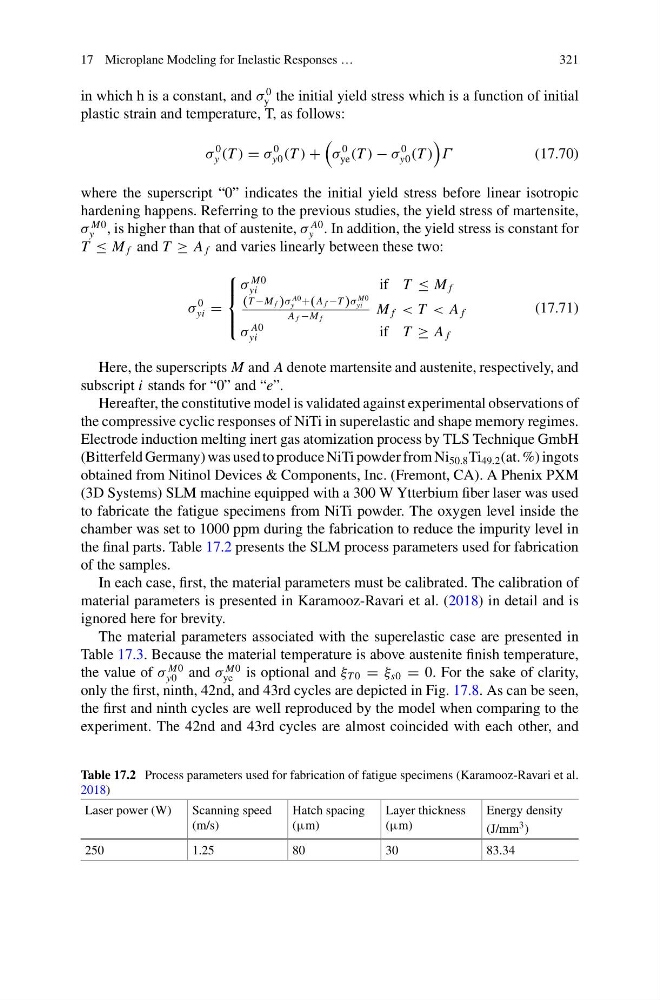
in which h is a constant, and σ
0
y the initial yield stress which is a function of initial
plastic strain and temperature, T, as follows:
σ
0
y (T ) = σ
0
y0 (T ) +
σ
0
ye (T ) − σ
0
y0 (T )
Γ
(17.70)
where the superscript “0” indicates the initial yield stress before linear isotropic
hardening happens. Referring to the previous studies, the yield stress of martensite,
σ
M0
y , is higher than that of austenite, σ
A0
y . In addition, the yield stress is constant for
T ≤ M f and T ≥ A f and varies linearly between these two:
σ
0
yi =
⎧
⎪ ⎨
⎪ ⎩
σ
M0
yi
if T ≤ M f
(T −M f )σ
A0
y +(A f −T )σ
M0
yi
A f −M f
M f < T < A f
σ
A0
yi
if T ≥ A f
(17.71)
Here, the superscripts M and A denote martensite and austenite, respectively, and
subscript i stands for “0” and “e”.
Hereafter, the constitutive model is validated against experimental observations of
the compressive cyclic responses of NiTi in superelastic and shape memory regimes.
Electrode induction melting inert gas atomization process by TLS Technique GmbH
(Bitterfeld Germany) was used to produce NiTi powder from Ni 50.8 Ti 49.2 (at. %) ingots
obtained from Nitinol Devices & Components, Inc. (Fremont, CA). A Phenix PXM
(3D Systems) SLM machine equipped with a 300 W Ytterbium fiber laser was used
to fabricate the fatigue specimens from NiTi powder. The oxygen level inside the
chamber was set to 1000 ppm during the fabrication to reduce the impurity level in
the final parts. Table 17.2 presents the SLM process parameters used for fabrication
of the samples.
In each case, first, the material parameters must be calibrated. The calibration of
material parameters is presented in Karamooz-Ravari et al. (2018) in detail and is
ignored here for brevity.
The material parameters associated with the superelastic case are presented in
Table 17.3. Because the material temperature is above austenite finish temperature,
the value of σ
M0
y0 and σ
M0
ye is optional and ξ T 0 = ξ s0 = 0. For the sake of clarity,
only the first, ninth, 42nd, and 43rd cycles are depicted in Fig. 17.8. As can be seen,
the first and ninth cycles are well reproduced by the model when comparing to the
experiment. The 42nd and 43rd cycles are almost coincided with each other, and
Table 17.2 Process parameters used for fabrication of fatigue specimens (Karamooz-Ravari et al.
2018)
Laser power (W)
Scanning speed
(m/s)
Hatch spacing
(µm)
Layer thickness
(µm)
Energy density
(J/mm 3 )
250
1.25
80
30
83.34