

2 Industrial Plant Oil Extraction
65
60
80
100 120 140 160
20
30
40
50
60
70
80
90
100
Yield (%)
temperature ( )
oil
saponin
0
1 0
2 0
3 0
4 0
5 0
6 0
30
40
50
60
70
80
90
100
Yield (%)
time (min)
oil
saponin
3:1
5:1 10:1 15:1 20:1 25:1
20
30
40
50
60
70
80
90
100
Yield (%)
liquid/solid ratio
oil
saponin
2
3
4
5
6
7
60
65
70
75
80
85
90
95
Yield (%)
oil
saponin
Pressure (MPa)
b
c
d
a
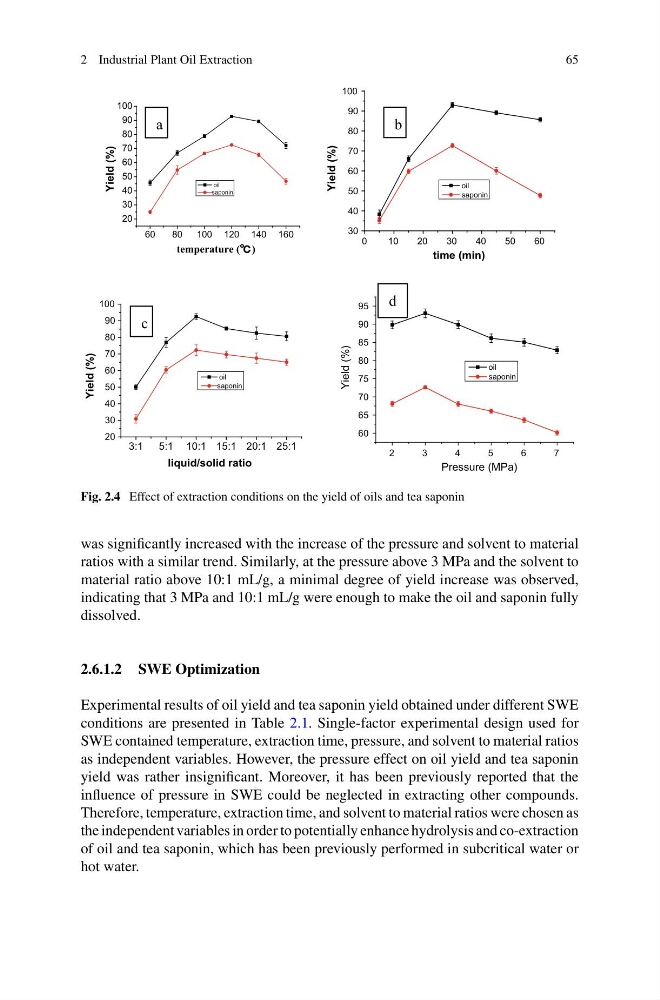
Fig. 2.4 Effect of extraction conditions on the yield of oils and tea saponin
was significantly increased with the increase of the pressure and solvent to material
ratios with a similar trend. Similarly, at the pressure above 3 MPa and the solvent to
material ratio above 10:1 mL/g, a minimal degree of yield increase was observed,
indicating that 3 MPa and 10:1 mL/g were enough to make the oil and saponin fully
dissolved.
2.6.1.2 SWE Optimization
Experimental results of oil yield and tea saponin yield obtained under different SWE
conditions are presented in Table 2.1. Single-factor experimental design used for
SWE contained temperature, extraction time, pressure, and solvent to material ratios
as independent variables. However, the pressure effect on oil yield and tea saponin
yield was rather insignificant. Moreover, it has been previously reported that the
influence of pressure in SWE could be neglected in extracting other compounds.
Therefore, temperature, extraction time, and solvent to material ratios were chosen as
the independent variables in order to potentially enhance hydrolysis and co-extraction
of oil and tea saponin, which has been previously performed in subcritical water or
hot water.
65
60
80
100 120 140 160
20
30
40
50
60
70
80
90
100
Yield (%)
temperature ( )
oil
saponin
0
1 0
2 0
3 0
4 0
5 0
6 0
30
40
50
60
70
80
90
100
Yield (%)
time (min)
oil
saponin
3:1
5:1 10:1 15:1 20:1 25:1
20
30
40
50
60
70
80
90
100
Yield (%)
liquid/solid ratio
oil
saponin
2
3
4
5
6
7
60
65
70
75
80
85
90
95
Yield (%)
oil
saponin
Pressure (MPa)
b
c
d
a
Fig. 2.4 Effect of extraction conditions on the yield of oils and tea saponin
was significantly increased with the increase of the pressure and solvent to material
ratios with a similar trend. Similarly, at the pressure above 3 MPa and the solvent to
material ratio above 10:1 mL/g, a minimal degree of yield increase was observed,
indicating that 3 MPa and 10:1 mL/g were enough to make the oil and saponin fully
dissolved.
2.6.1.2 SWE Optimization
Experimental results of oil yield and tea saponin yield obtained under different SWE
conditions are presented in Table 2.1. Single-factor experimental design used for
SWE contained temperature, extraction time, pressure, and solvent to material ratios
as independent variables. However, the pressure effect on oil yield and tea saponin
yield was rather insignificant. Moreover, it has been previously reported that the
influence of pressure in SWE could be neglected in extracting other compounds.
Therefore, temperature, extraction time, and solvent to material ratios were chosen as
the independent variables in order to potentially enhance hydrolysis and co-extraction
of oil and tea saponin, which has been previously performed in subcritical water or
hot water.