

6 Tool Model Building and Research on Cutting Simulation …
71
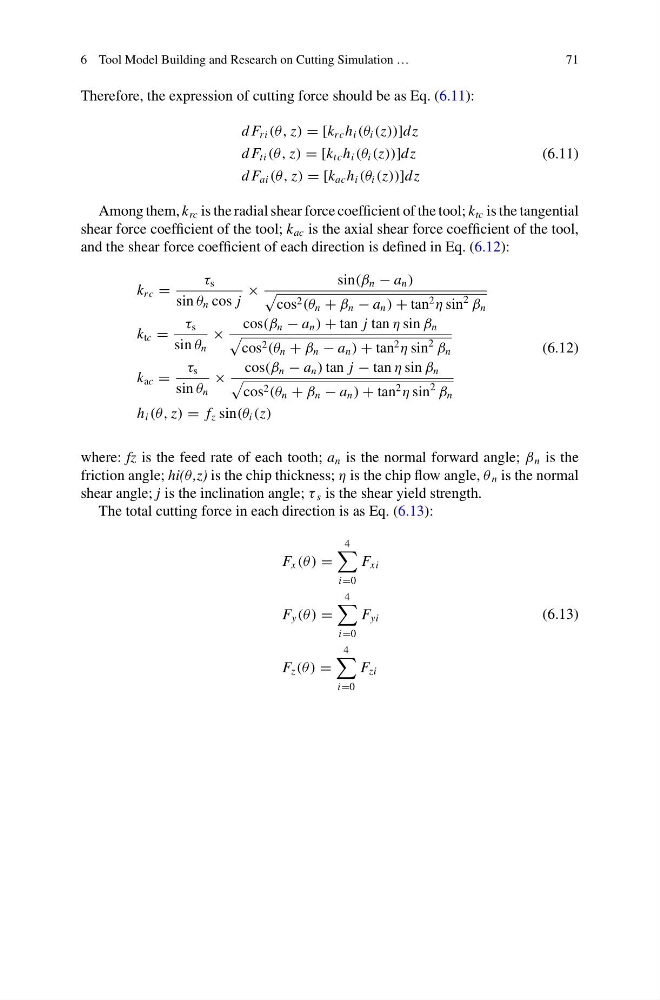
Therefore, the expression of cutting force should be as Eq. (6.11):
d F ri (θ, z) = [k rc h i (θ i (z))]dz
d F ti (θ, z) = [k tc h i (θ i (z))]dz
d F ai (θ, z) = [k ac h i (θ i (z))]dz
(6.11)
Among them, k rc is the radial shear force coefficient of the tool; k tc is the tangential
shear force coefficient of the tool; k ac is the axial shear force coefficient of the tool,
and the shear force coefficient of each direction is defined in Eq. (6.12):
k rc =
τ s
sin θ n cos j
×
sin(β n − a n )
cos 2 (θ n + β n − a n ) + tan 2 η sin
2
β n
k tc =
τ s
sin θ n
×
cos(β n − a n ) + tan j tan η sin β n
cos 2 (θ n + β n − a n ) + tan 2 η sin
2
β n
k ac =
τ s
sin θ n
×
cos(β n − a n ) tan j − tan η sin β n
cos 2 (θ n + β n − a n ) + tan 2 η sin
2
β n
h i (θ, z) = f z sin(θ i (z)
(6.12)
where: fz is the feed rate of each tooth; a n is the normal forward angle; β n is the
friction angle; hi(θ ,z) is the chip thickness; η is the chip flow angle, θ n is the normal
shear angle; j is the inclination angle; τ s is the shear yield strength.
The total cutting force in each direction is as Eq. (6.13):
F x (θ ) =
4
i=0
F xi
F y (θ ) =
4
i=0
F yi
F z (θ ) =
4
i=0
F zi
(6.13)