

186
S. Ruan et al.
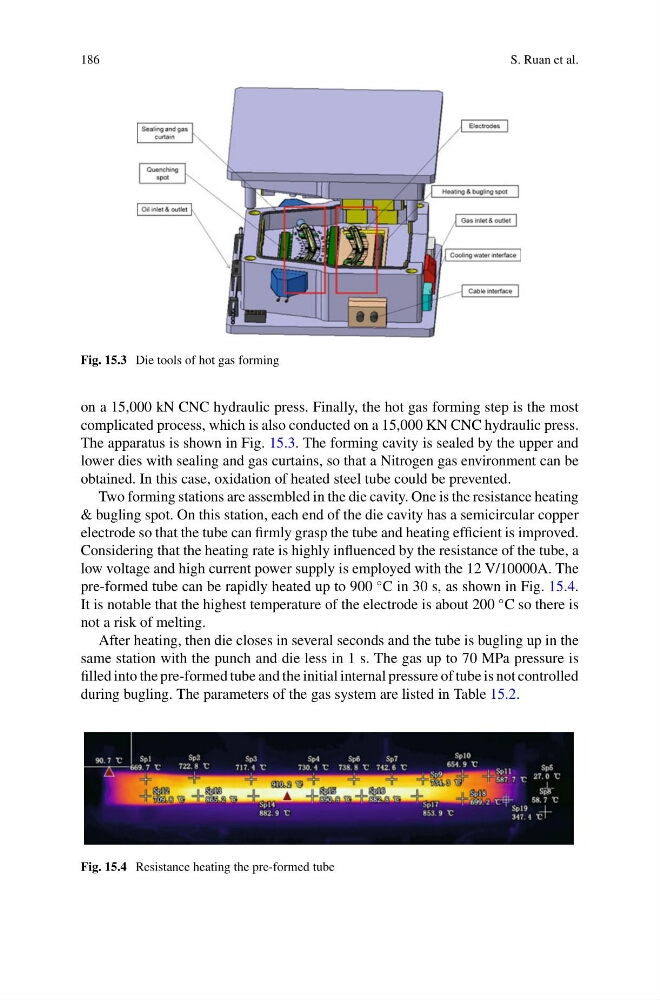
Fig. 15.3 Die tools of hot gas forming
on a 15,000 kN CNC hydraulic press. Finally, the hot gas forming step is the most
complicated process, which is also conducted on a 15,000 KN CNC hydraulic press.
The apparatus is shown in Fig. 15.3. The forming cavity is sealed by the upper and
lower dies with sealing and gas curtains, so that a Nitrogen gas environment can be
obtained. In this case, oxidation of heated steel tube could be prevented.
Two forming stations are assembled in the die cavity. One is the resistance heating
& bugling spot. On this station, each end of the die cavity has a semicircular copper
electrode so that the tube can firmly grasp the tube and heating efficient is improved.
Considering that the heating rate is highly influenced by the resistance of the tube, a
low voltage and high current power supply is employed with the 12 V/10000A. The
pre-formed tube can be rapidly heated up to 900
◦ C in 30 s, as shown in Fig. 15.4.
It is notable that the highest temperature of the electrode is about 200
◦ C so there is
not a risk of melting.
After heating, then die closes in several seconds and the tube is bugling up in the
same station with the punch and die less in 1 s. The gas up to 70 MPa pressure is
filled into the pre-formed tube and the initial internal pressure of tube is not controlled
during bugling. The parameters of the gas system are listed in Table 15.2.
Fig. 15.4 Resistance heating the pre-formed tube