

15 Simulation of Multi-step Tube Hot Gas Forming Process …
185
15.2 Indirect Hot Gas Forming of a Torsion Beam
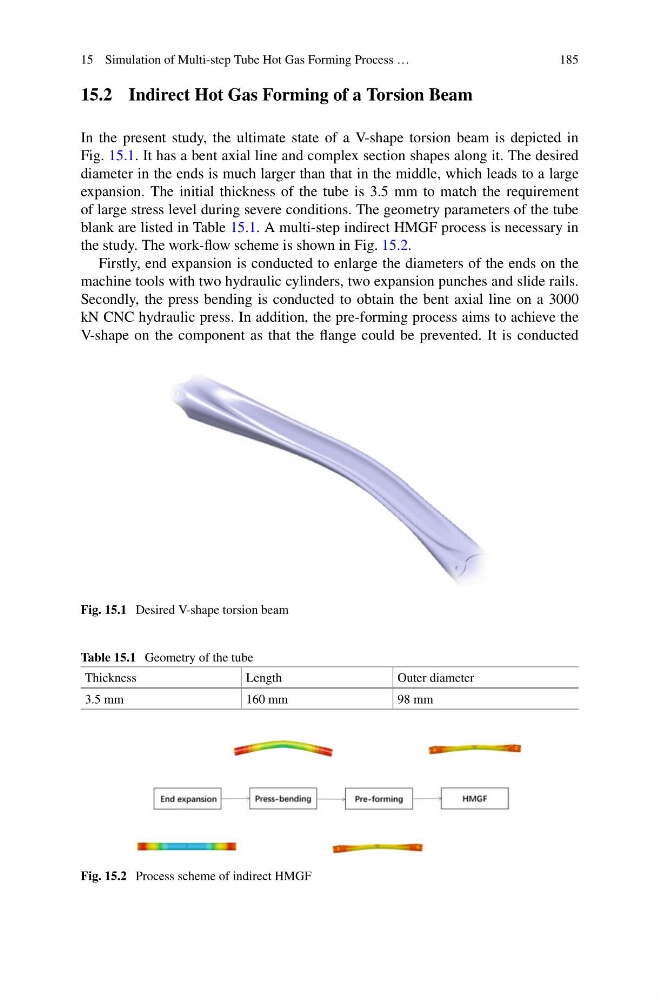
In the present study, the ultimate state of a V-shape torsion beam is depicted in
Fig. 15.1. It has a bent axial line and complex section shapes along it. The desired
diameter in the ends is much larger than that in the middle, which leads to a large
expansion. The initial thickness of the tube is 3.5 mm to match the requirement
of large stress level during severe conditions. The geometry parameters of the tube
blank are listed in Table 15.1. A multi-step indirect HMGF process is necessary in
the study. The work-flow scheme is shown in Fig. 15.2.
Firstly, end expansion is conducted to enlarge the diameters of the ends on the
machine tools with two hydraulic cylinders, two expansion punches and slide rails.
Secondly, the press bending is conducted to obtain the bent axial line on a 3000
kN CNC hydraulic press. In addition, the pre-forming process aims to achieve the
V-shape on the component as that the flange could be prevented. It is conducted
Fig. 15.1 Desired V-shape torsion beam
Table 15.1 Geometry of the tube
Thickness
Length
Outer diameter
3.5 mm
160 mm
98 mm
Fig. 15.2 Process scheme of indirect HMGF