

Depending on the production facilities and the electrolyte composition,
electrodeposited nickel canb er elativelyh ard( 120–400 HV). Despite
competition from hard chromium and electroless nickel,e lectrodeposited
nickel is still beingu sed as an engineering coating because of its relatively
low price. Some of its properties are:
1. Good general corrosion resistance
2. Good protection from fretting corrosion
3. Good machineability
4. The ability of layerso f5 0–75 m mt op revent scaling at high
temperatures
5. Mechanical properties, including the internal stress and hardness,
thata re variablea nd that canb efi xedb ys electingt he
manufacturing parameters
6. Excellent combination with chromium layers
7. Ac ertain porosity
8. At endencyf or layer thicknesses below1 0–20 m mo ns teel to give
corrosion spots because of porosity
The electrodeposition can be eitherd irectly on steel or over an intermediate coating of copper. Copper is used as an underlayment to facilitate
buffing, because it is softer than steel, and to increase the required coating
thickness with am aterial less expensive than nickel.
The mostp opular electroless nickel plating process is the one where
hypophosphite is used as the reducer. Autocatalytic nickel ion reduction by
hypophosphite takesp lace in botha cid and alkaline solutions. In as table
solutionw ith ah ighc oating quality,t he deposition rate may be as high as
20–25 m m/h. However,ar elatively high temperature of 1948 F/908 Ci s
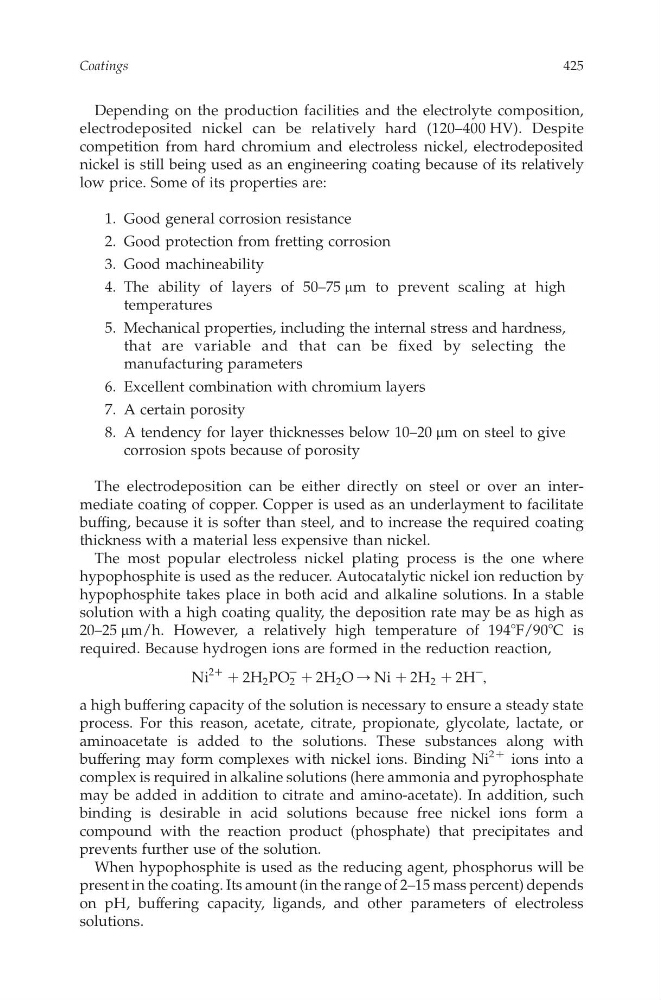
required. Because hydrogen ions are formed in the reduction reaction,
Ni
2 C C 2H 2 PO
K
2 C 2H 2 O / Ni C 2H 2 C 2H
K
;
ahigh buffering capacity of the solutionisnecessary to ensure asteady state
process. For this reason, acetate, citrate, propionate, glycolate, lactate, or
aminoacetate is added to the solutions. These substances alongw ith
buffering may form complexesw ith nickel ions. Binding Ni
2 C
ionsi nto a
complex is requiredinalkaline solutions (here ammonia and pyrophosphate
may be added in addition to citrate and amino-acetate). In addition,s uch
binding is desirable in acid solutions because free nickel ionsf orm a
compound with the reaction product (phosphate) that precipitates and
prevents further use of the solution.
When hypophosphite is used as the reducing agent, phosphorus will be
present in the coating. Its amount (in the rangeof2–15 mass percent) depends
on pH,b uffering capacity,l igands, and other parameterso fe lectroless
solutions.
Coatings
425
CAT8247—CHAPTER 7—17/10/2006—15:02—TRGANESH—XMLM ODEL B–pp. 403–485