

The EZINEX ® Process for Secondary Zinc Bearing Materials
791
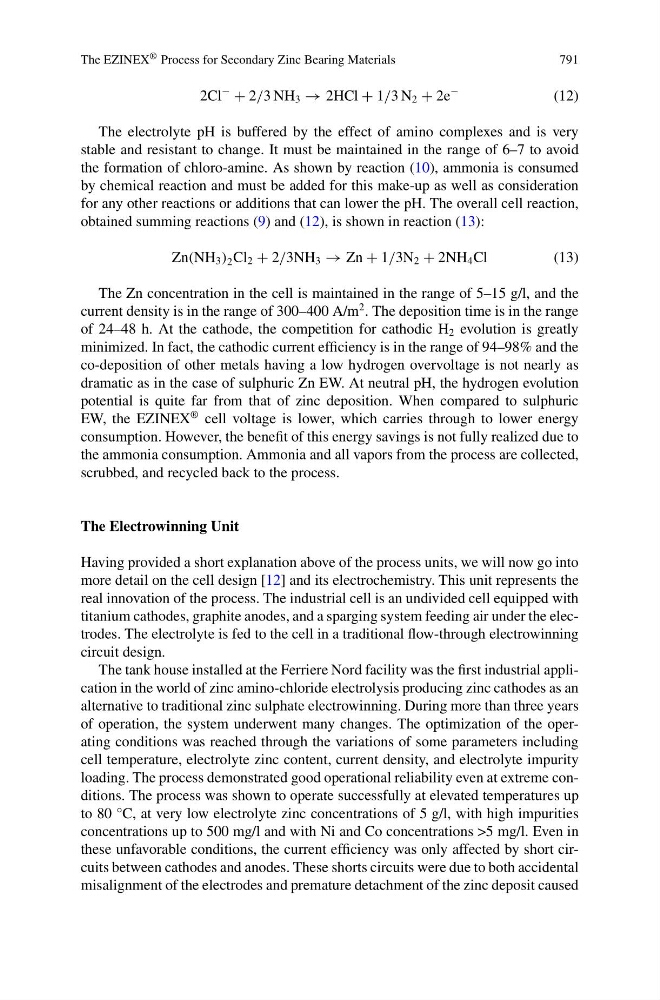
2Cl
−
+ 2/3 NH 3 → 2HCl + 1/3 N 2 + 2e
−
(12)
The electrolyte pH is buffered by the effect of amino complexes and is very
stable and resistant to change. It must be maintained in the range of 6–7 to avoid
the formation of chloro-amine. As shown by reaction (10), ammonia is consumed
by chemical reaction and must be added for this make-up as well as consideration
for any other reactions or additions that can lower the pH. The overall cell reaction,
obtained summing reactions (9) and (12), is shown in reaction (13):
Zn(NH 3 ) 2 Cl 2 + 2/3NH 3 → Zn + 1/3N 2 + 2NH 4 Cl
(13)
The Zn concentration in the cell is maintained in the range of 5–15 g/l, and the
current density is in the range of 300–400 A/m
2 . The deposition time is in the range
of 24–48 h. At the cathode, the competition for cathodic H 2 evolution is greatly
minimized. In fact, the cathodic current efficiency is in the range of 94–98% and the
co-deposition of other metals having a low hydrogen overvoltage is not nearly as
dramatic as in the case of sulphuric Zn EW. At neutral pH, the hydrogen evolution
potential is quite far from that of zinc deposition. When compared to sulphuric
EW, the EZINEX
® cell voltage is lower, which carries through to lower energy
consumption. However, the benefit of this energy savings is not fully realized due to
the ammonia consumption. Ammonia and all vapors from the process are collected,
scrubbed, and recycled back to the process.
The Electrowinning Unit
Having provided a short explanation above of the process units, we will now go into
more detail on the cell design [12] and its electrochemistry. This unit represents the
real innovation of the process. The industrial cell is an undivided cell equipped with
titanium cathodes, graphite anodes, and a sparging system feeding air under the electrodes. The electrolyte is fed to the cell in a traditional flow-through electrowinning
circuit design.
The tank house installed at the Ferriere Nord facility was the first industrial application in the world of zinc amino-chloride electrolysis producing zinc cathodes as an
alternative to traditional zinc sulphate electrowinning. During more than three years
of operation, the system underwent many changes. The optimization of the operating conditions was reached through the variations of some parameters including
cell temperature, electrolyte zinc content, current density, and electrolyte impurity
loading. The process demonstrated good operational reliability even at extreme conditions. The process was shown to operate successfully at elevated temperatures up
to 80 °C, at very low electrolyte zinc concentrations of 5 g/l, with high impurities
concentrations up to 500 mg/l and with Ni and Co concentrations >5 mg/l. Even in
these unfavorable conditions, the current efficiency was only affected by short circuits between cathodes and anodes. These shorts circuits were due to both accidental
misalignment of the electrodes and premature detachment of the zinc deposit caused