

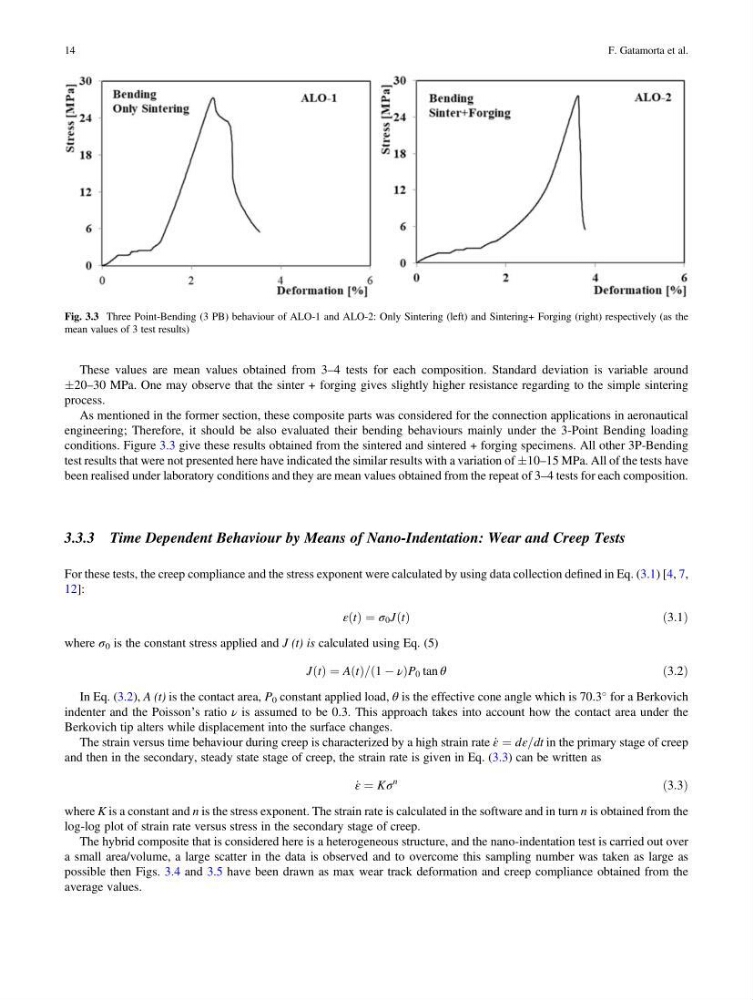
These values are mean values obtained from 3–4 tests for each composition. Standard deviation is variable around
Æ20–30 MPa. One may observe that the sinter + forging gives slightly higher resistance regarding to the simple sintering
process.
As mentioned in the former section, these composite parts was considered for the connection applications in aeronautical
engineering; Therefore, it should be also evaluated their bending behaviours mainly under the 3-Point Bending loading
conditions. Figure 3.3 give these results obtained from the sintered and sintered + forging specimens. All other 3P-Bending
test results that were not presented here have indicated the similar results with a variation of Æ10–15 MPa. All of the tests have
been realised under laboratory conditions and they are mean values obtained from the repeat of 3–4 tests for each composition.
3.3.3 Time Dependent Behaviour by Means of Nano-Indentation: Wear and Creep Tests
For these tests, the creep compliance and the stress exponent were calculated by using data collection defined in Eq. (3.1) [4, 7,
12]:
ε t
ð Þ ¼ σ 0 J t
ð Þ
ð3:1Þ
where σ 0 is the constant stress applied and J (t) is calculated using Eq. (5)
J t
ð Þ ¼ A t
ð Þ= 1 À ν
ð
ÞP 0 tan θ
ð3:2Þ
In Eq. (3.2), A (t) is the contact area, P 0 constant applied load, θ is the effective cone angle which is 70.3
for a Berkovich
indenter and the Poisson’s ratio ν is assumed to be 0.3. This approach takes into account how the contact area under the
Berkovich tip alters while displacement into the surface changes.
The strain versus time behaviour during creep is characterized by a high strain rate _
ε ¼ dε=dt in the primary stage of creep
and then in the secondary, steady state stage of creep, the strain rate is given in Eq. (3.3) can be written as
_
ε ¼ Kσ
n
ð3:3Þ
where K is a constant and n is the stress exponent. The strain rate is calculated in the software and in turn n is obtained from the
log-log plot of strain rate versus stress in the secondary stage of creep.
The hybrid composite that is considered here is a heterogeneous structure, and the nano-indentation test is carried out over
a small area/volume, a large scatter in the data is observed and to overcome this sampling number was taken as large as
possible then Figs. 3.4 and 3.5 have been drawn as max wear track deformation and creep compliance obtained from the
average values.
Fig. 3.3 Three Point-Bending (3 PB) behaviour of ALO-1 and ALO-2: Only Sintering (left) and Sintering+ Forging (right) respectively (as the
mean values of 3 test results)
14
F. Gatamorta et al.