

506
S. K. Sinha et al.
I =
π × d
4
64
=
3.14 × 12
4
64
= 1.017 × 10
−9 m
4
(15)
Substituting above values in Eq. (6),
σ b =
M × y
I
=
1128.38 × 6 × 10
−3
1.017 × 10 −9
= 6.651 MPa
(16)
Considering factor of safety as 4, maximum allowable tensile stress (σ A ) becomes
210 MPa. Comparing σ A Eq. (16),
σ b < σ A
(17)
4 Fabrication of Parts
Fabrication of parts was the most important part of the project as effort was made to
construct the roti maker with locally available raw material procured at an economical
rate, and fabrication work was carried out with a semi-skilled approach, all of which
was carried out in the college workshop with all necessary tools used being tools that
are available at any workshop. Operations carried out are as following:
4.1 Cutting
Cutting of the M.S. square pipe was done by accurately measuring the section lengths.
Marking was done with the help of L square ruler and scribber, and then cutting
operation was performed in a 2200 W cutoff saw machine with no load speed of
3800 RPM. The abrasive cutter was having diameter 14 inches and 2.8 mm thick
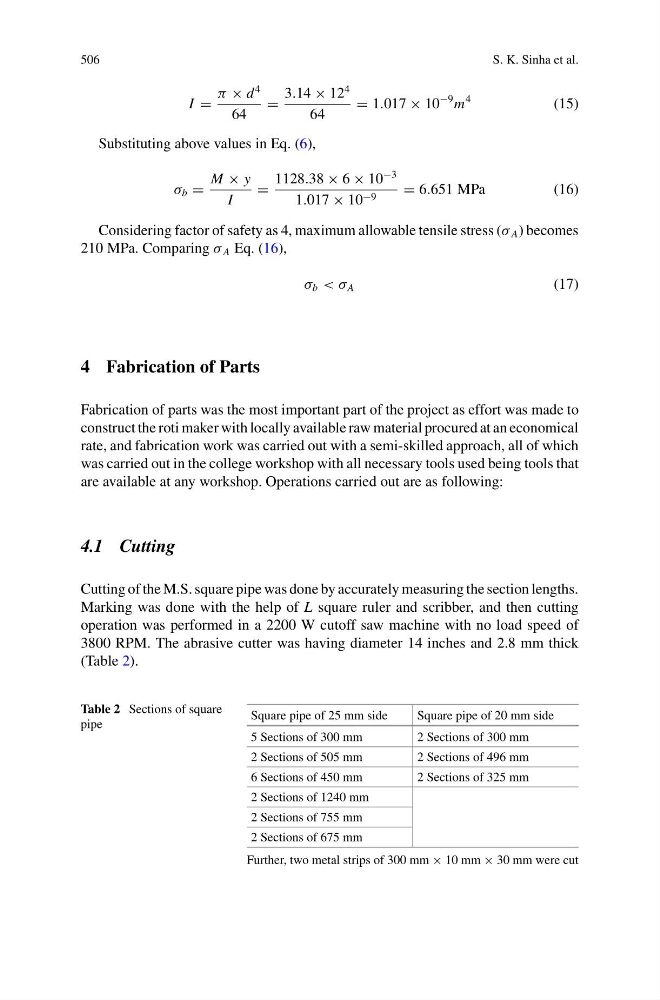
(Table 2).
Table 2 Sections of square
pipe
Square pipe of 25 mm side
Square pipe of 20 mm side
5 Sections of 300 mm
2 Sections of 300 mm
2 Sections of 505 mm
2 Sections of 496 mm
6 Sections of 450 mm
2 Sections of 325 mm
2 Sections of 1240 mm
2 Sections of 755 mm
2 Sections of 675 mm
Further, two metal strips of 300 mm × 10 mm × 30 mm were cut