

An Effect of Process Parameter on Physical Appearance …
115
0
3
6
9
12
15
18
21
24
27
30
Avg.
Thick
Avg.
Width
2000
2200
2400
0
3
6
9
12
15
18
21
24
27
30
Avg.
Thick
Avg.
Width
20
25
30
0
3
6
9
12
15
18
21
24
27
30
Avg.
Thick
Avg.
Width
0°
1°
2°
Rotation speed in RPM
Travel speed in mm/min
Tilting of Head in degree
a
b
c
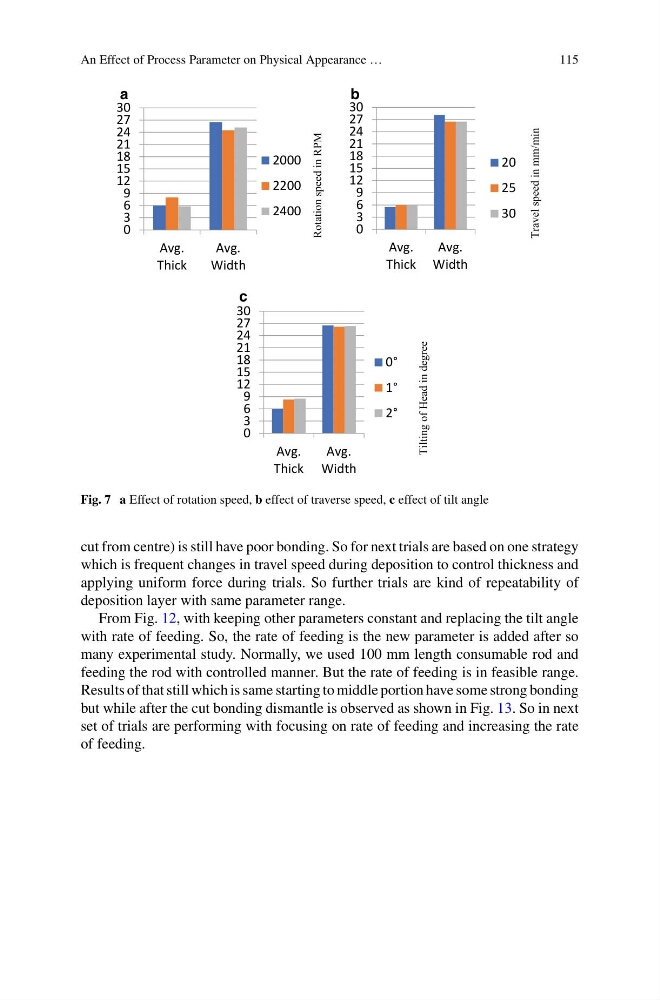
Fig. 7 a Effect of rotation speed, b effect of traverse speed, c effect of tilt angle
cut from centre) is still have poor bonding. So for next trials are based on one strategy
which is frequent changes in travel speed during deposition to control thickness and
applying uniform force during trials. So further trials are kind of repeatability of
deposition layer with same parameter range.
From Fig. 12, with keeping other parameters constant and replacing the tilt angle
with rate of feeding. So, the rate of feeding is the new parameter is added after so
many experimental study. Normally, we used 100 mm length consumable rod and
feeding the rod with controlled manner. But the rate of feeding is in feasible range.
Results of that still which is same starting to middle portion have some strong bonding
but while after the cut bonding dismantle is observed as shown in Fig. 13. So in next
set of trials are performing with focusing on rate of feeding and increasing the rate
of feeding.