

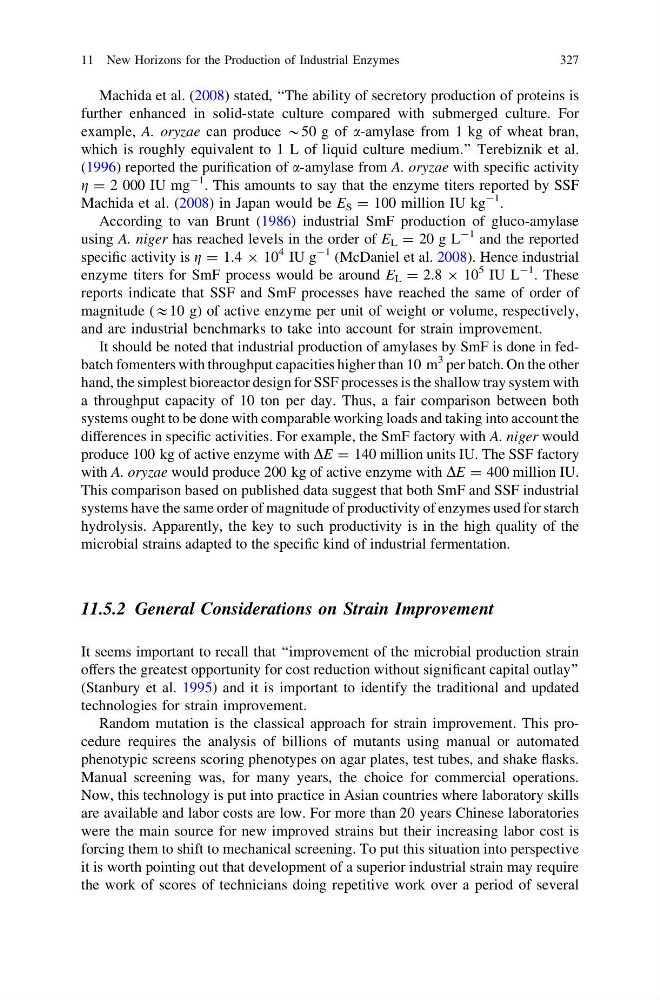
Machida et al. (2008) stated, ‘‘The ability of secretory production of proteins is
further enhanced in solid-state culture compared with submerged culture. For
example, A. oryzae can produce *50 g of a-amylase from 1 kg of wheat bran,
which is roughly equivalent to 1 L of liquid culture medium.’’ Terebiznik et al.
(1996) reported the purification of a-amylase from A. oryzae with specific activity
g = 2 000 IU mg
-1 . This amounts to say that the enzyme titers reported by SSF
Machida et al. (2008) in Japan would be E S = 100 million IU kg
-1 .
According to van Brunt (1986) industrial SmF production of gluco-amylase
using A. niger has reached levels in the order of E L = 20 g L
-1 and the reported
specific activity is g = 1.4 9 10
4 IU g
-1 (McDaniel et al. 2008). Hence industrial
enzyme titers for SmF process would be around E L = 2.8 9 10
5 IU L
-1 . These
reports indicate that SSF and SmF processes have reached the same of order of
magnitude (&10 g) of active enzyme per unit of weight or volume, respectively,
and are industrial benchmarks to take into account for strain improvement.
It should be noted that industrial production of amylases by SmF is done in fedbatch fomenters with throughput capacities higher than 10 m
3 per batch. On the other
hand, the simplest bioreactor design for SSF processes is the shallow tray system with
a throughput capacity of 10 ton per day. Thus, a fair comparison between both
systems ought to be done with comparable working loads and taking into account the
differences in specific activities. For example, the SmF factory with A. niger would
produce 100 kg of active enzyme with DE = 140 million units IU. The SSF factory
with A. oryzae would produce 200 kg of active enzyme with DE = 400 million IU.
This comparison based on published data suggest that both SmF and SSF industrial
systems have the same order of magnitude of productivity of enzymes used for starch
hydrolysis. Apparently, the key to such productivity is in the high quality of the
microbial strains adapted to the specific kind of industrial fermentation.
11.5.2 General Considerations on Strain Improvement
It seems important to recall that ‘‘improvement of the microbial production strain
offers the greatest opportunity for cost reduction without significant capital outlay’’
(Stanbury et al. 1995) and it is important to identify the traditional and updated
technologies for strain improvement.
Random mutation is the classical approach for strain improvement. This procedure requires the analysis of billions of mutants using manual or automated
phenotypic screens scoring phenotypes on agar plates, test tubes, and shake flasks.
Manual screening was, for many years, the choice for commercial operations.
Now, this technology is put into practice in Asian countries where laboratory skills
are available and labor costs are low. For more than 20 years Chinese laboratories
were the main source for new improved strains but their increasing labor cost is
forcing them to shift to mechanical screening. To put this situation into perspective
it is worth pointing out that development of a superior industrial strain may require
the work of scores of technicians doing repetitive work over a period of several
11 New Horizons for the Production of Industrial Enzymes
327